Siding, Siding and More Siding!
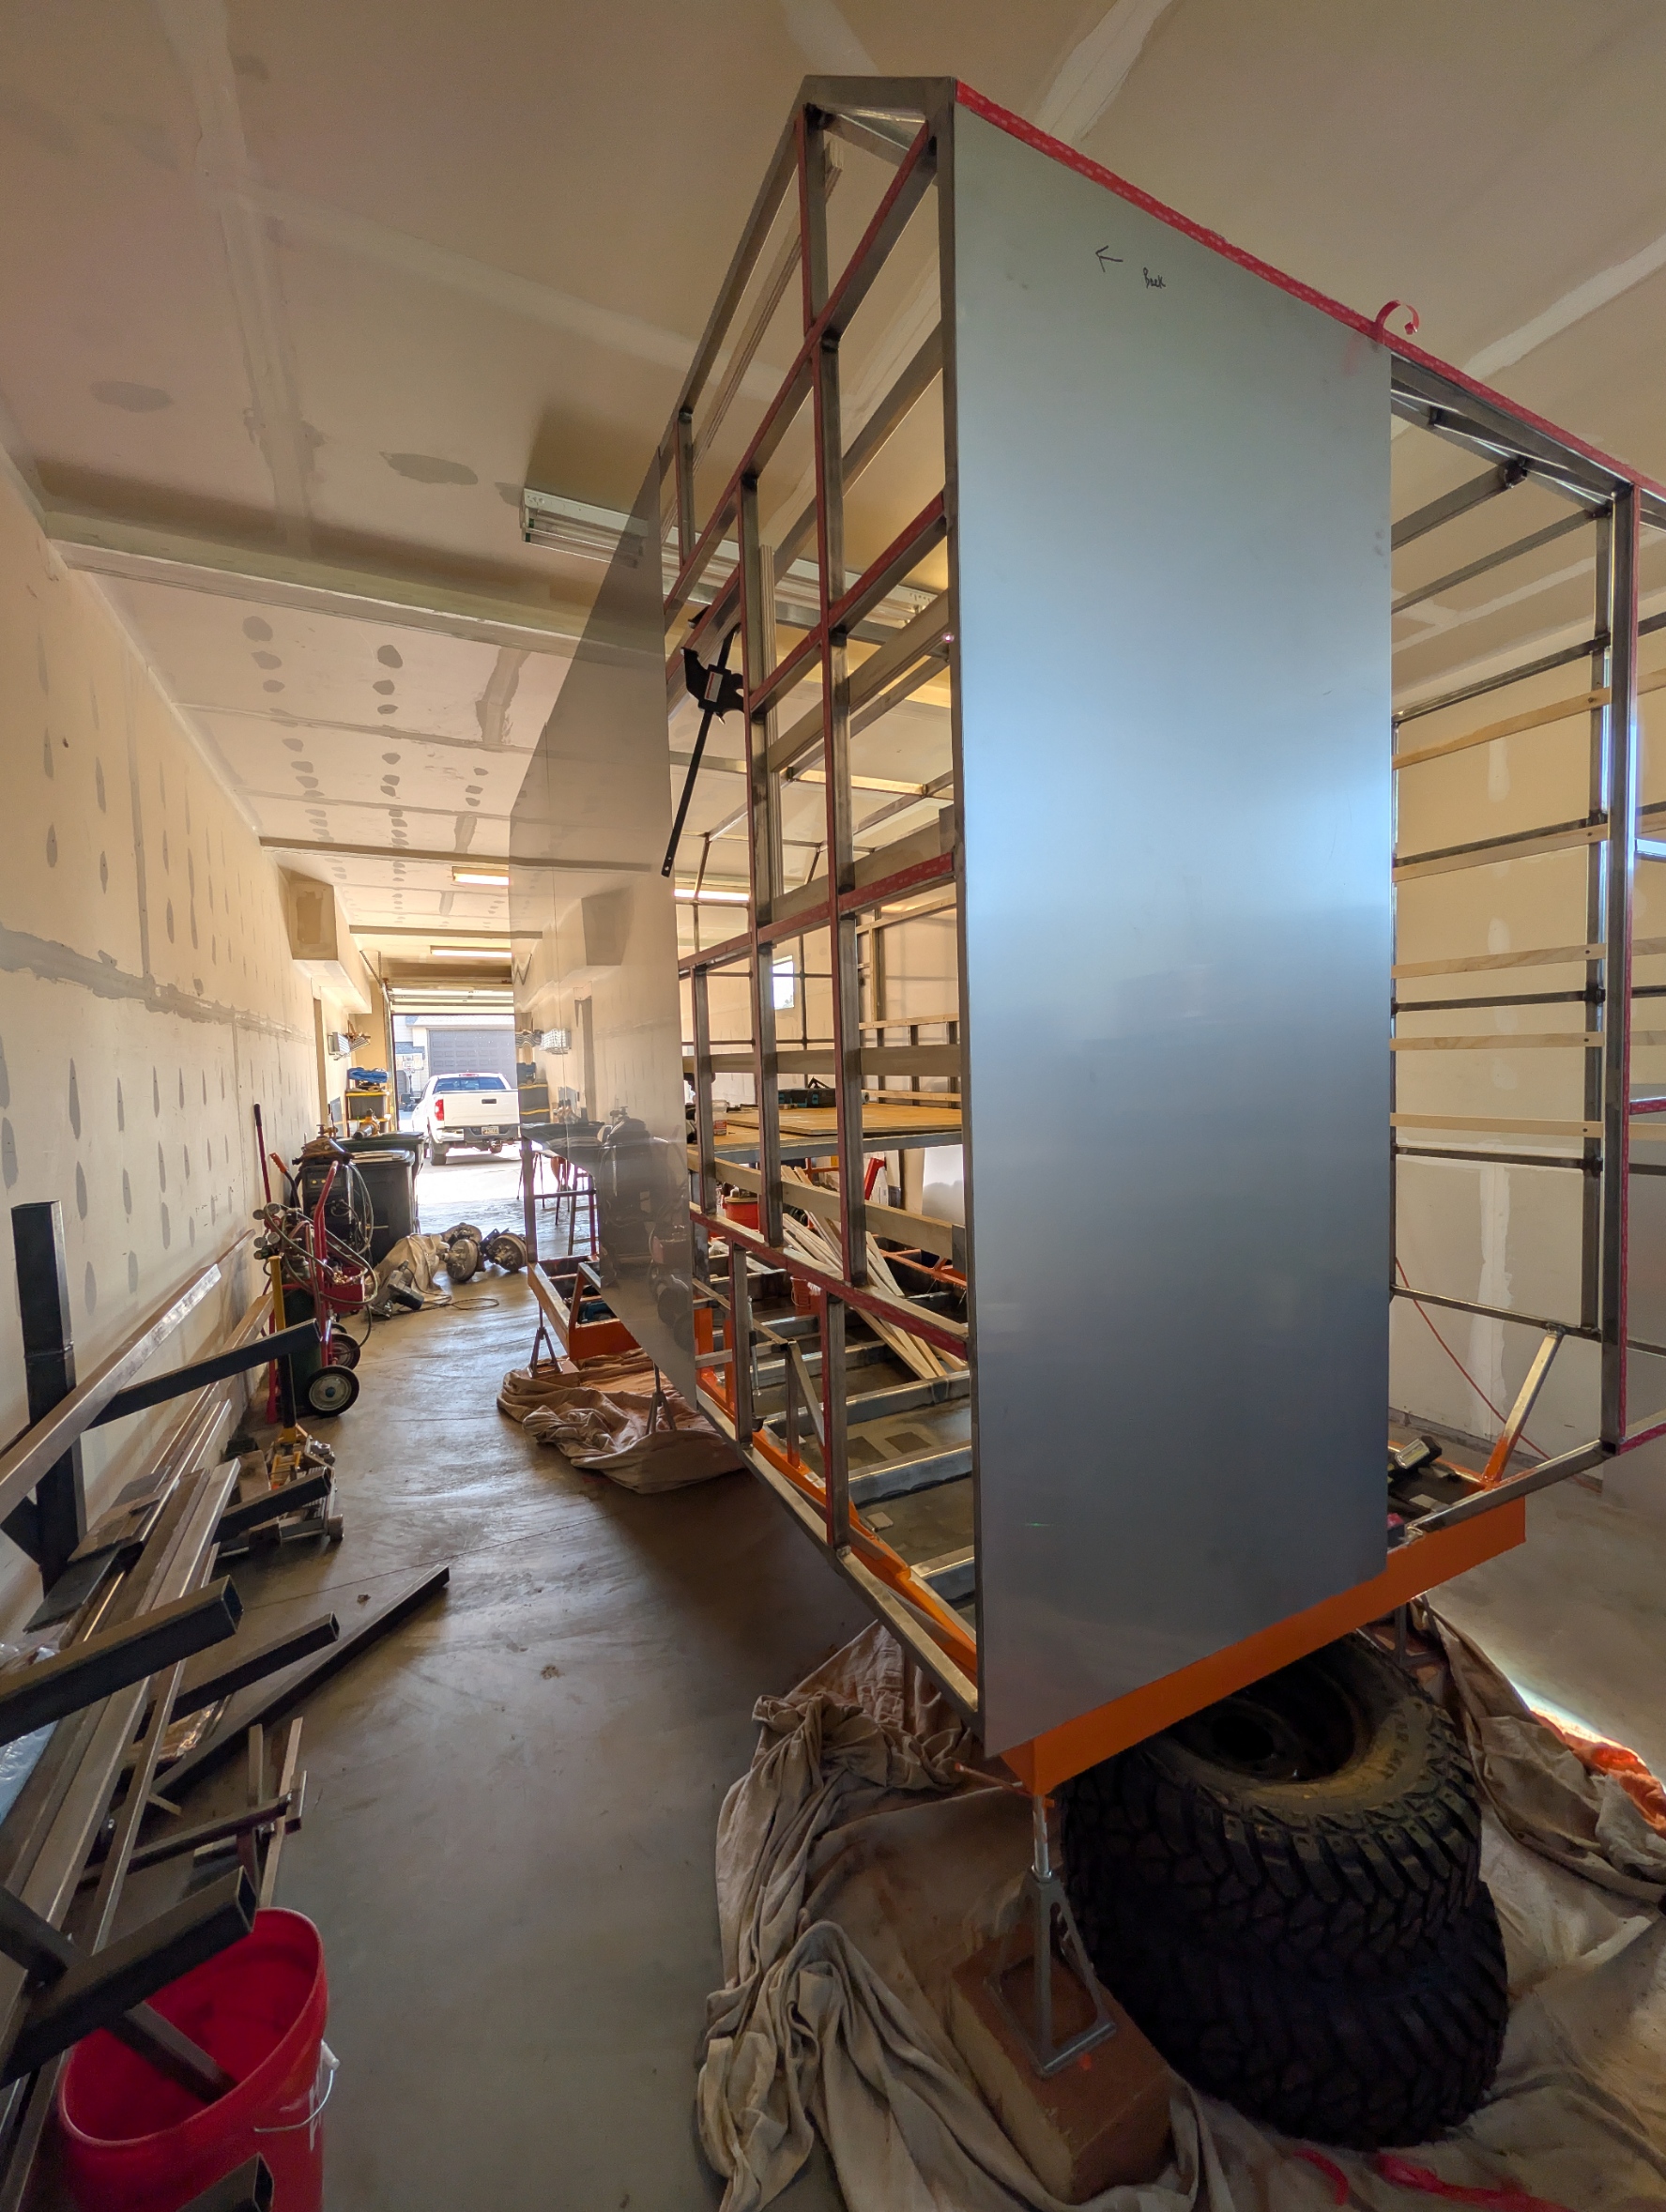
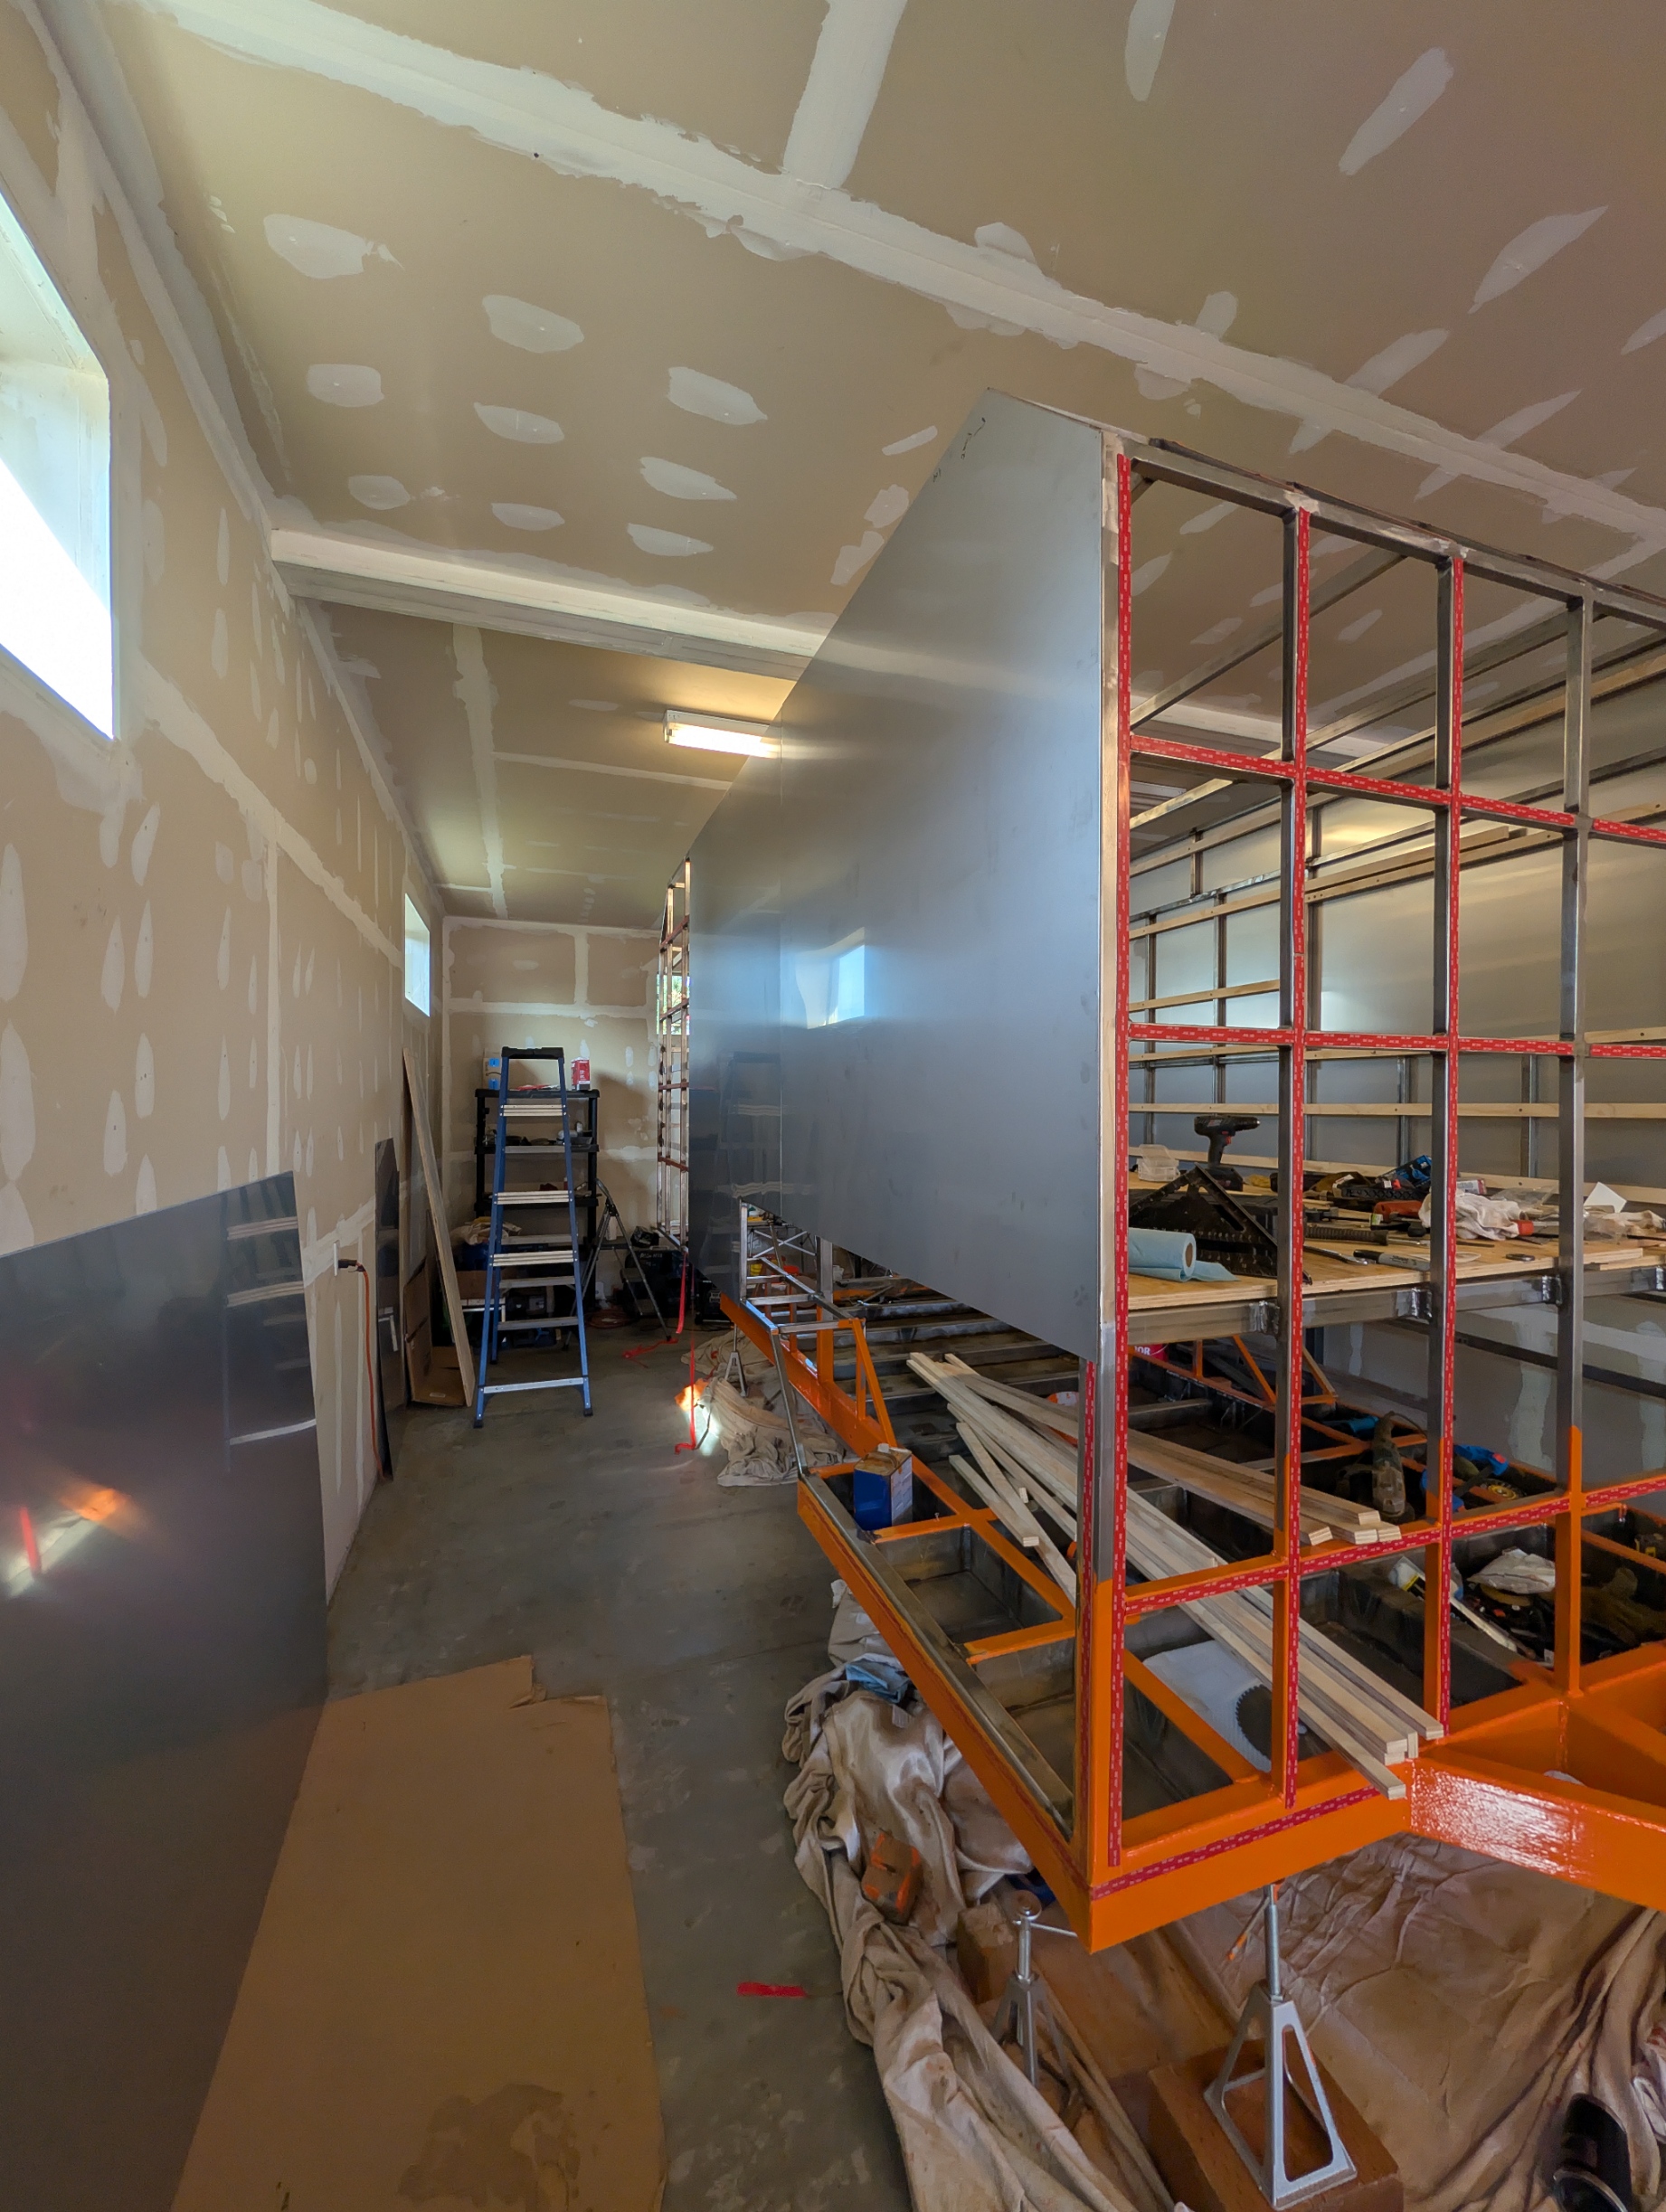
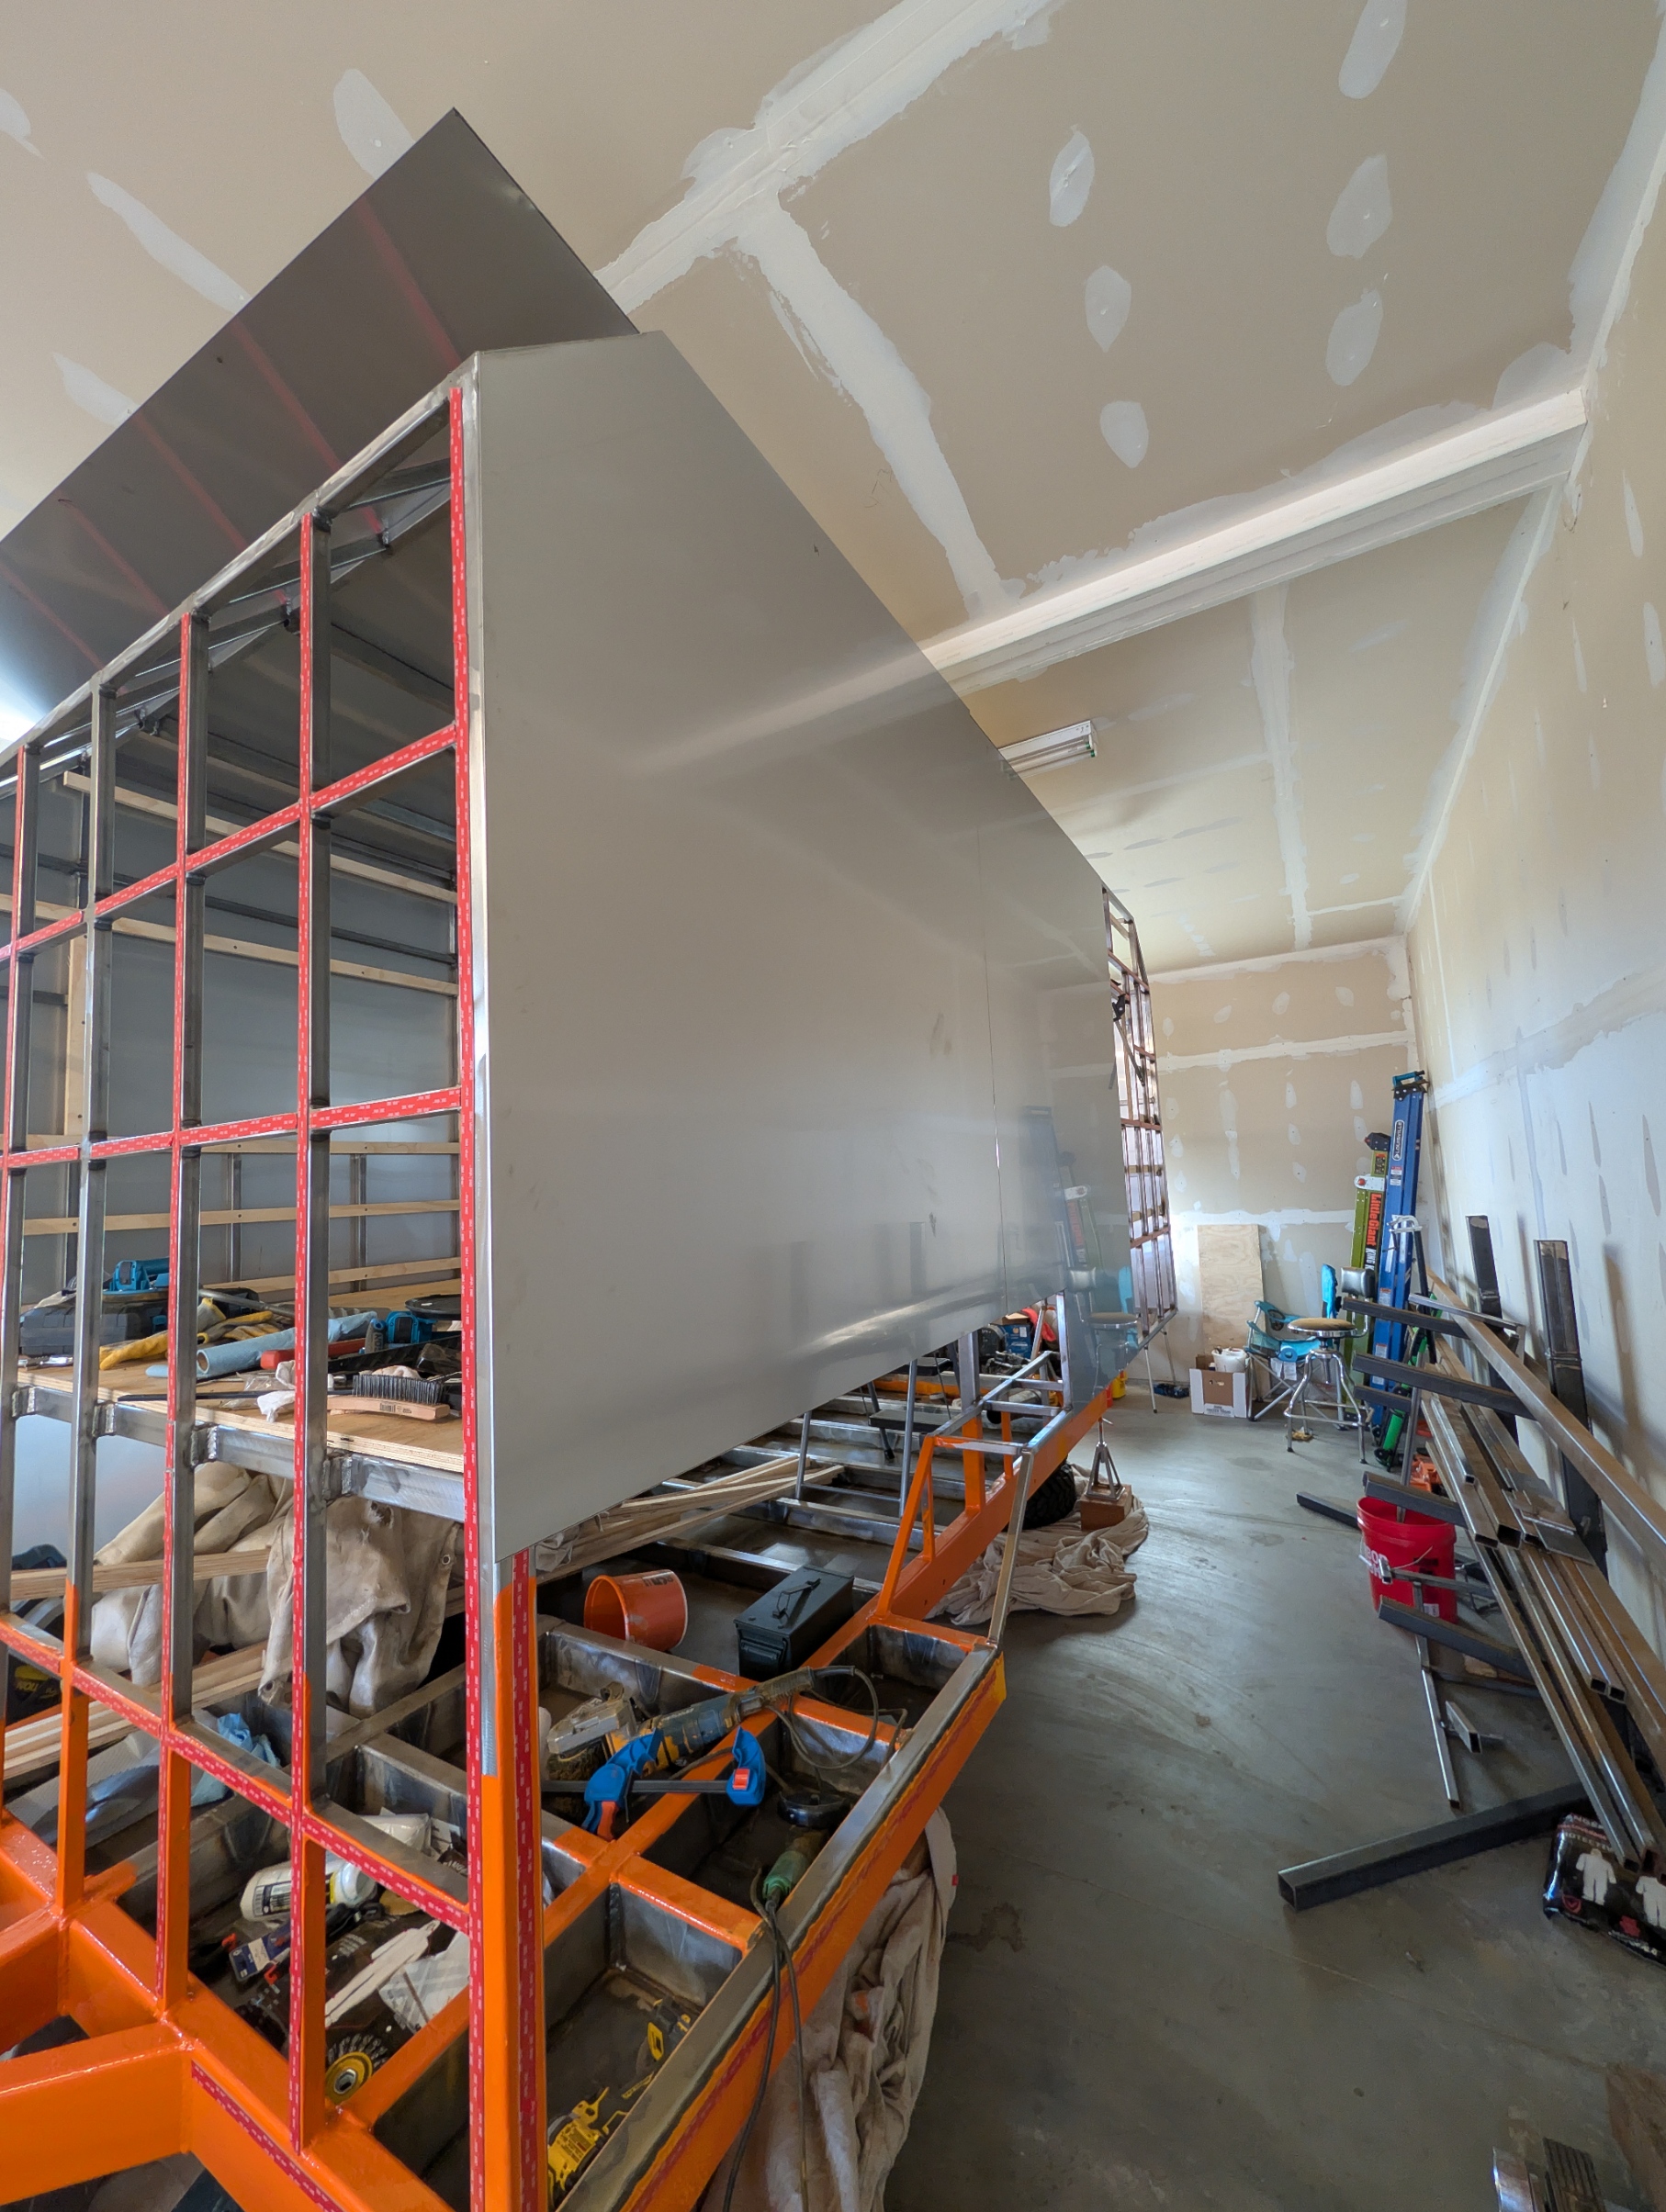
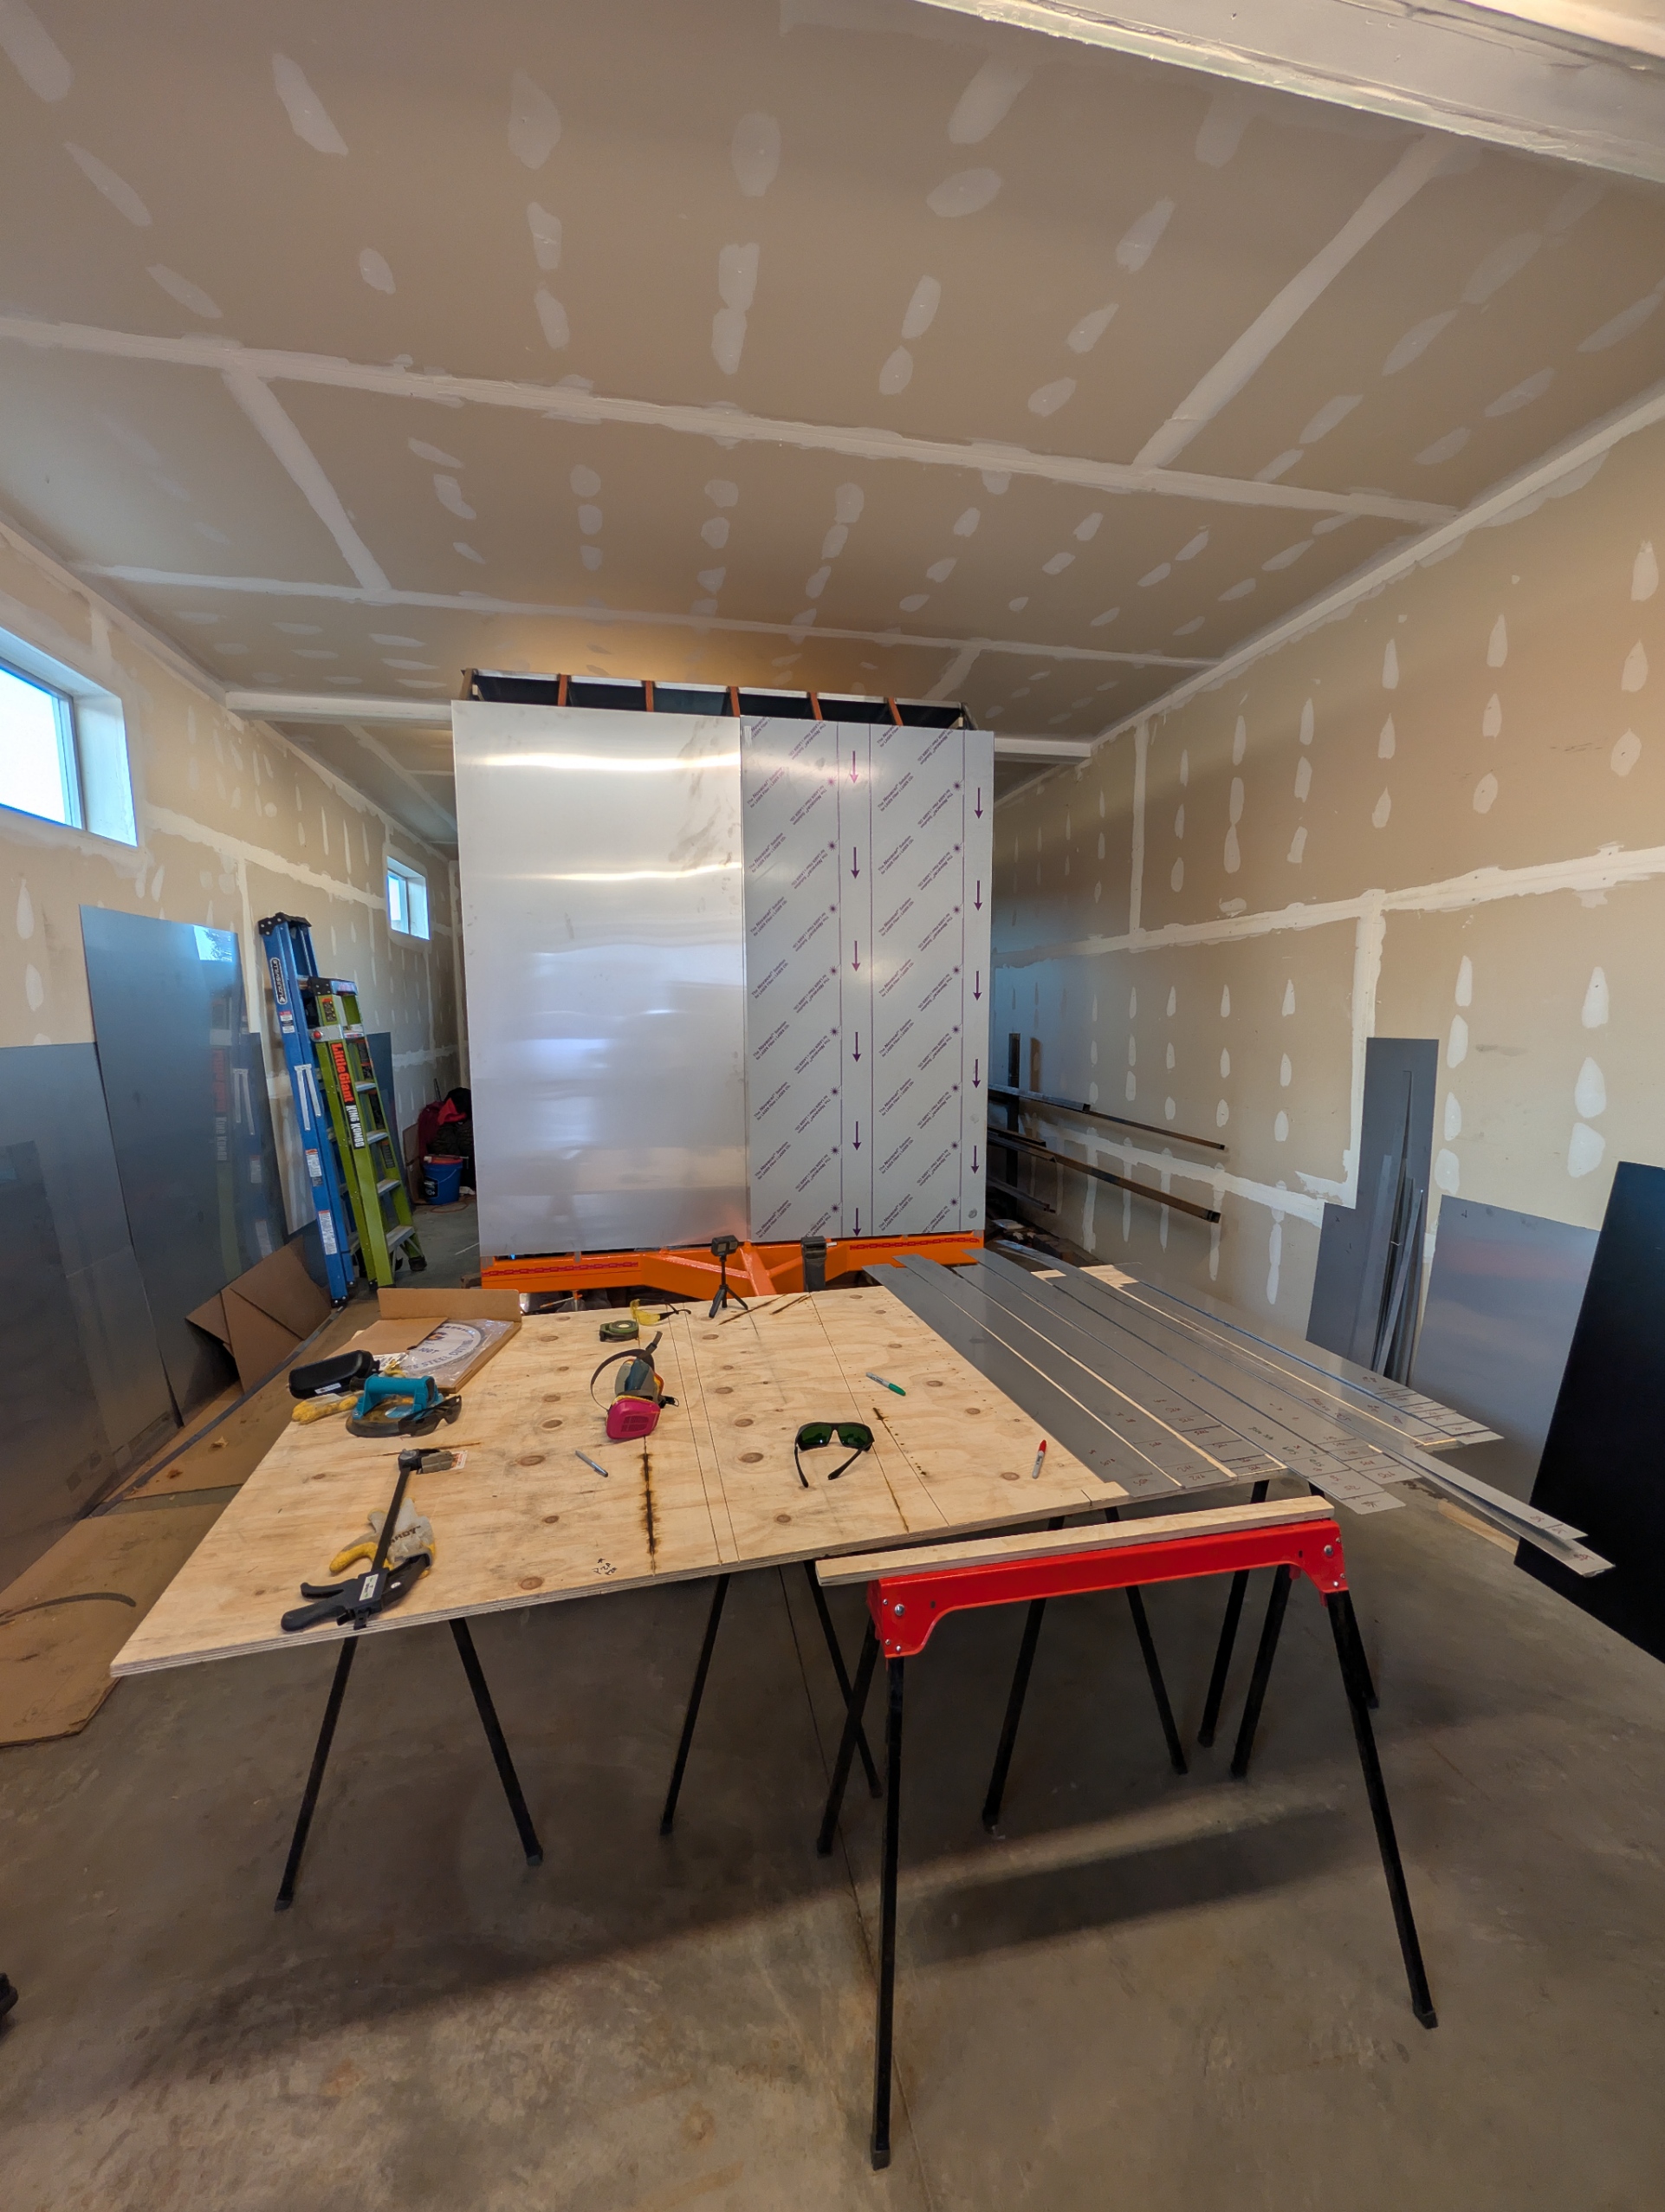
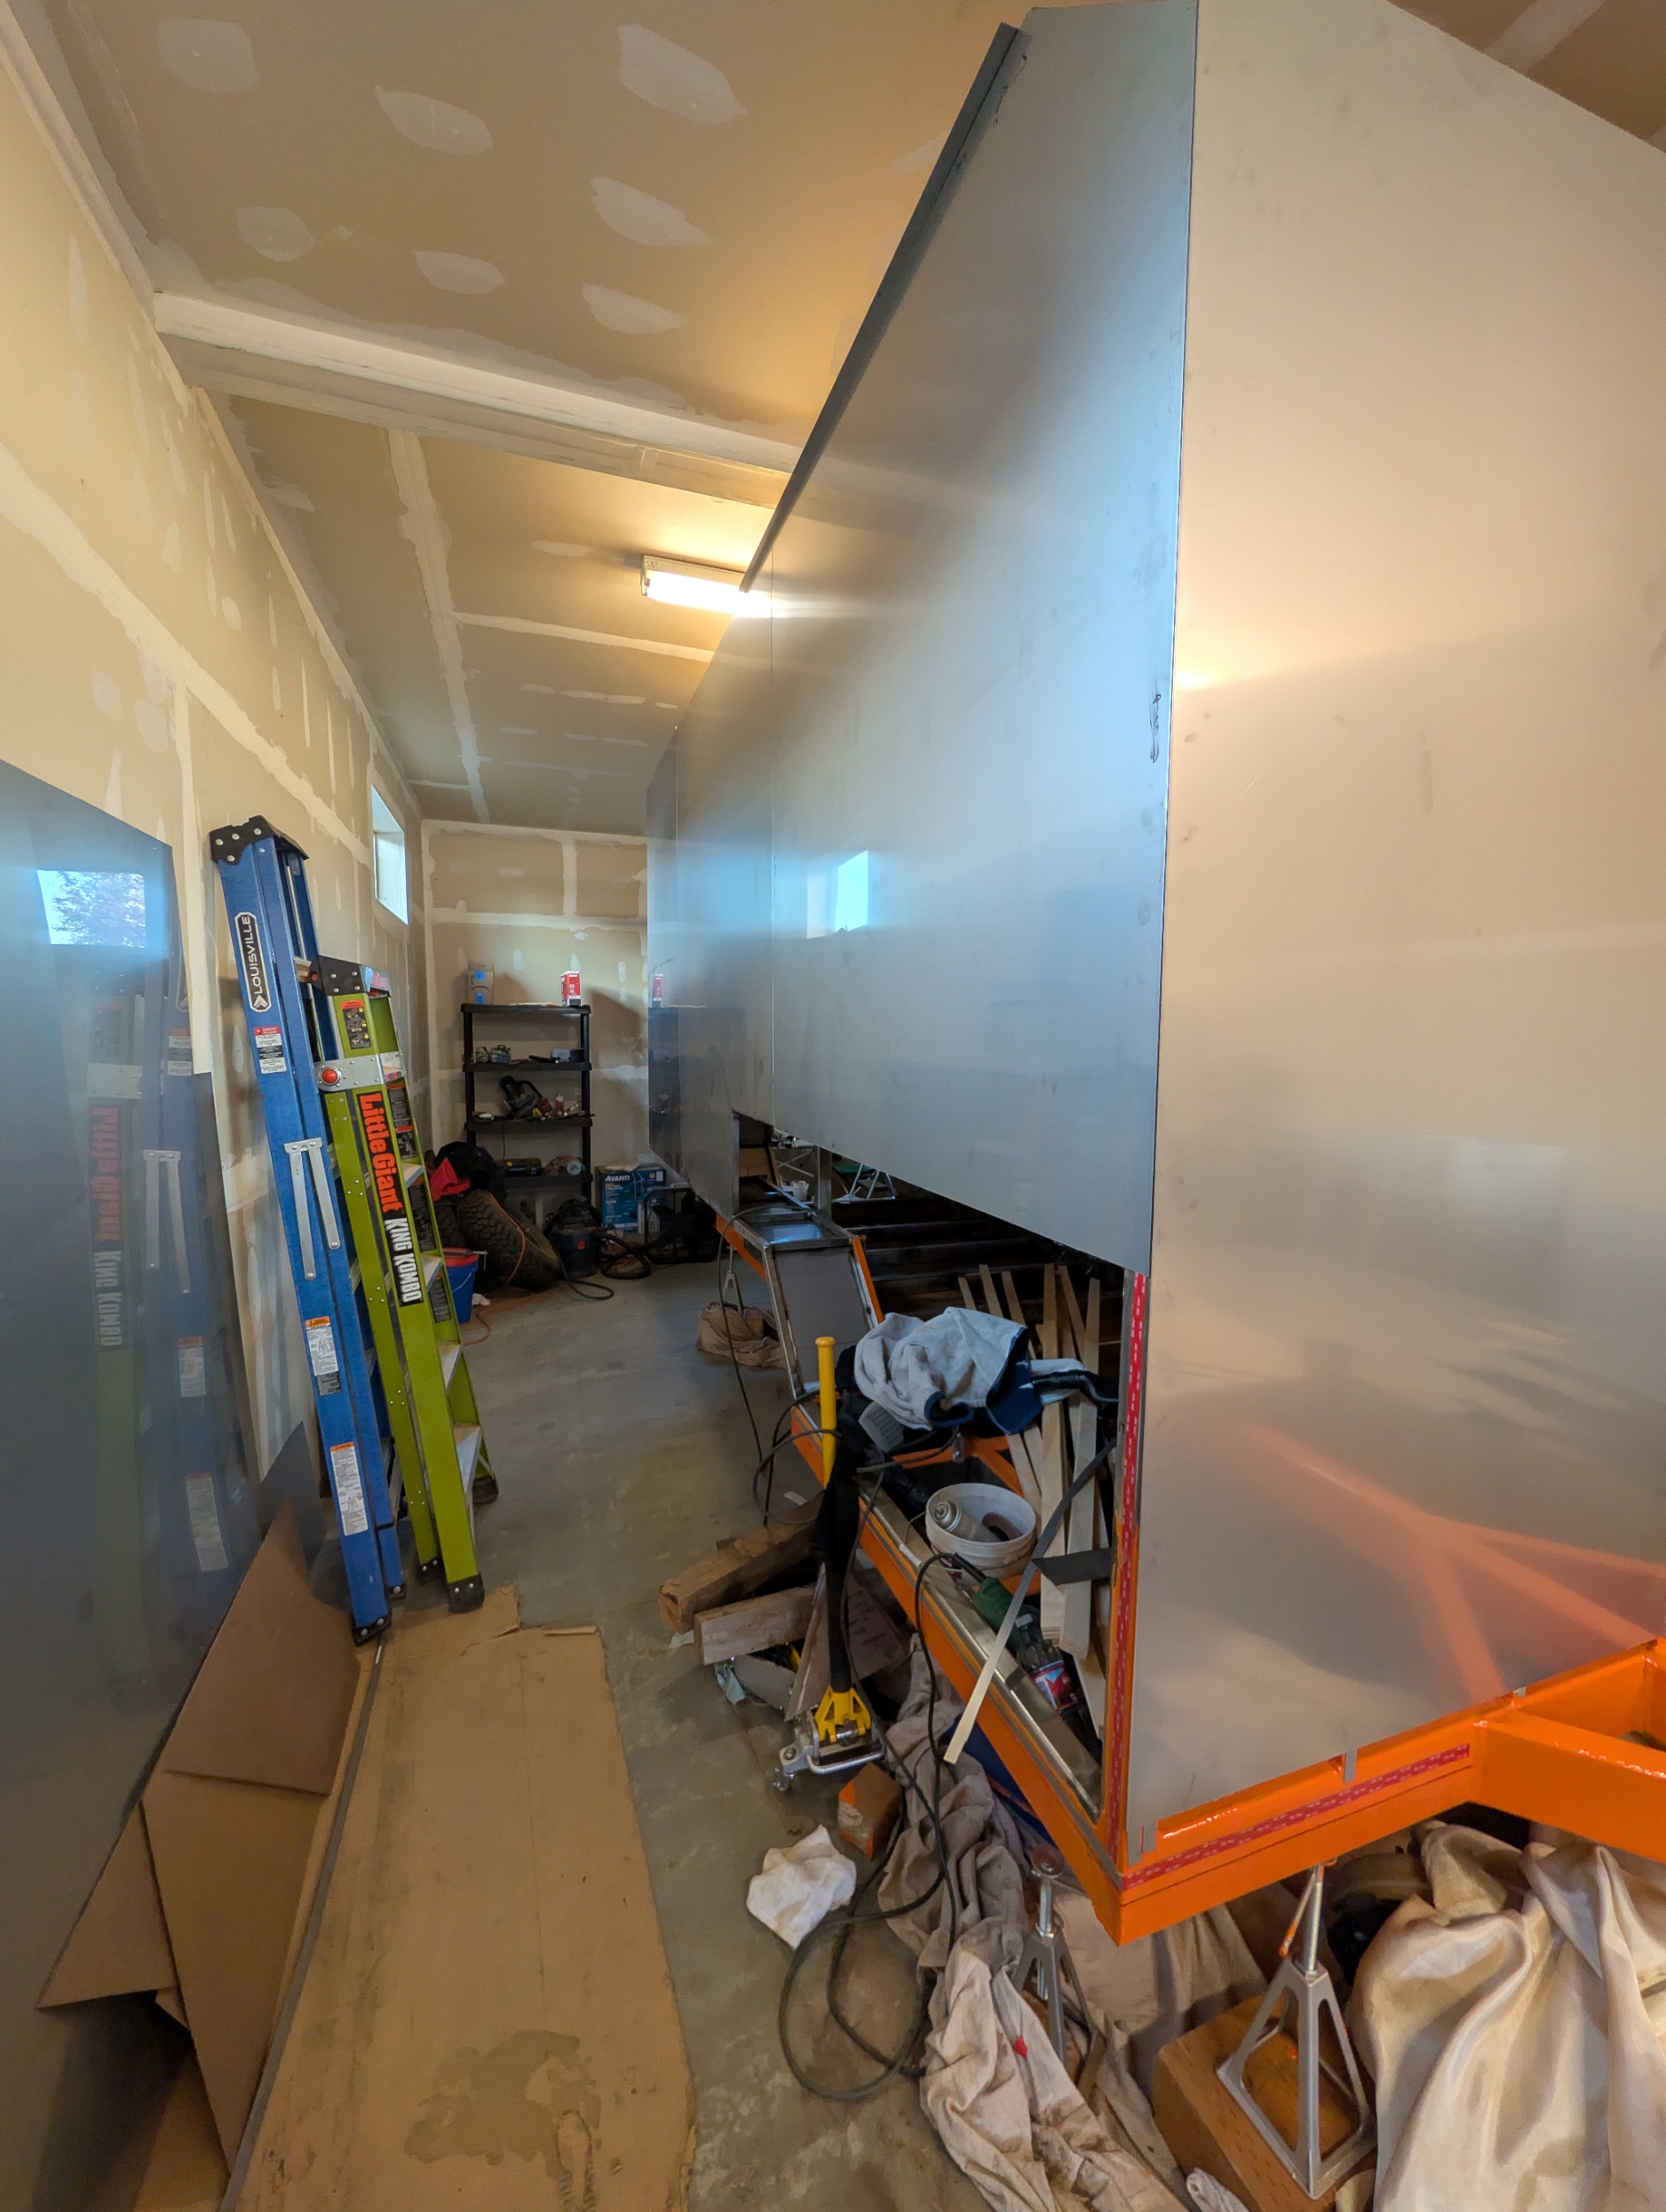
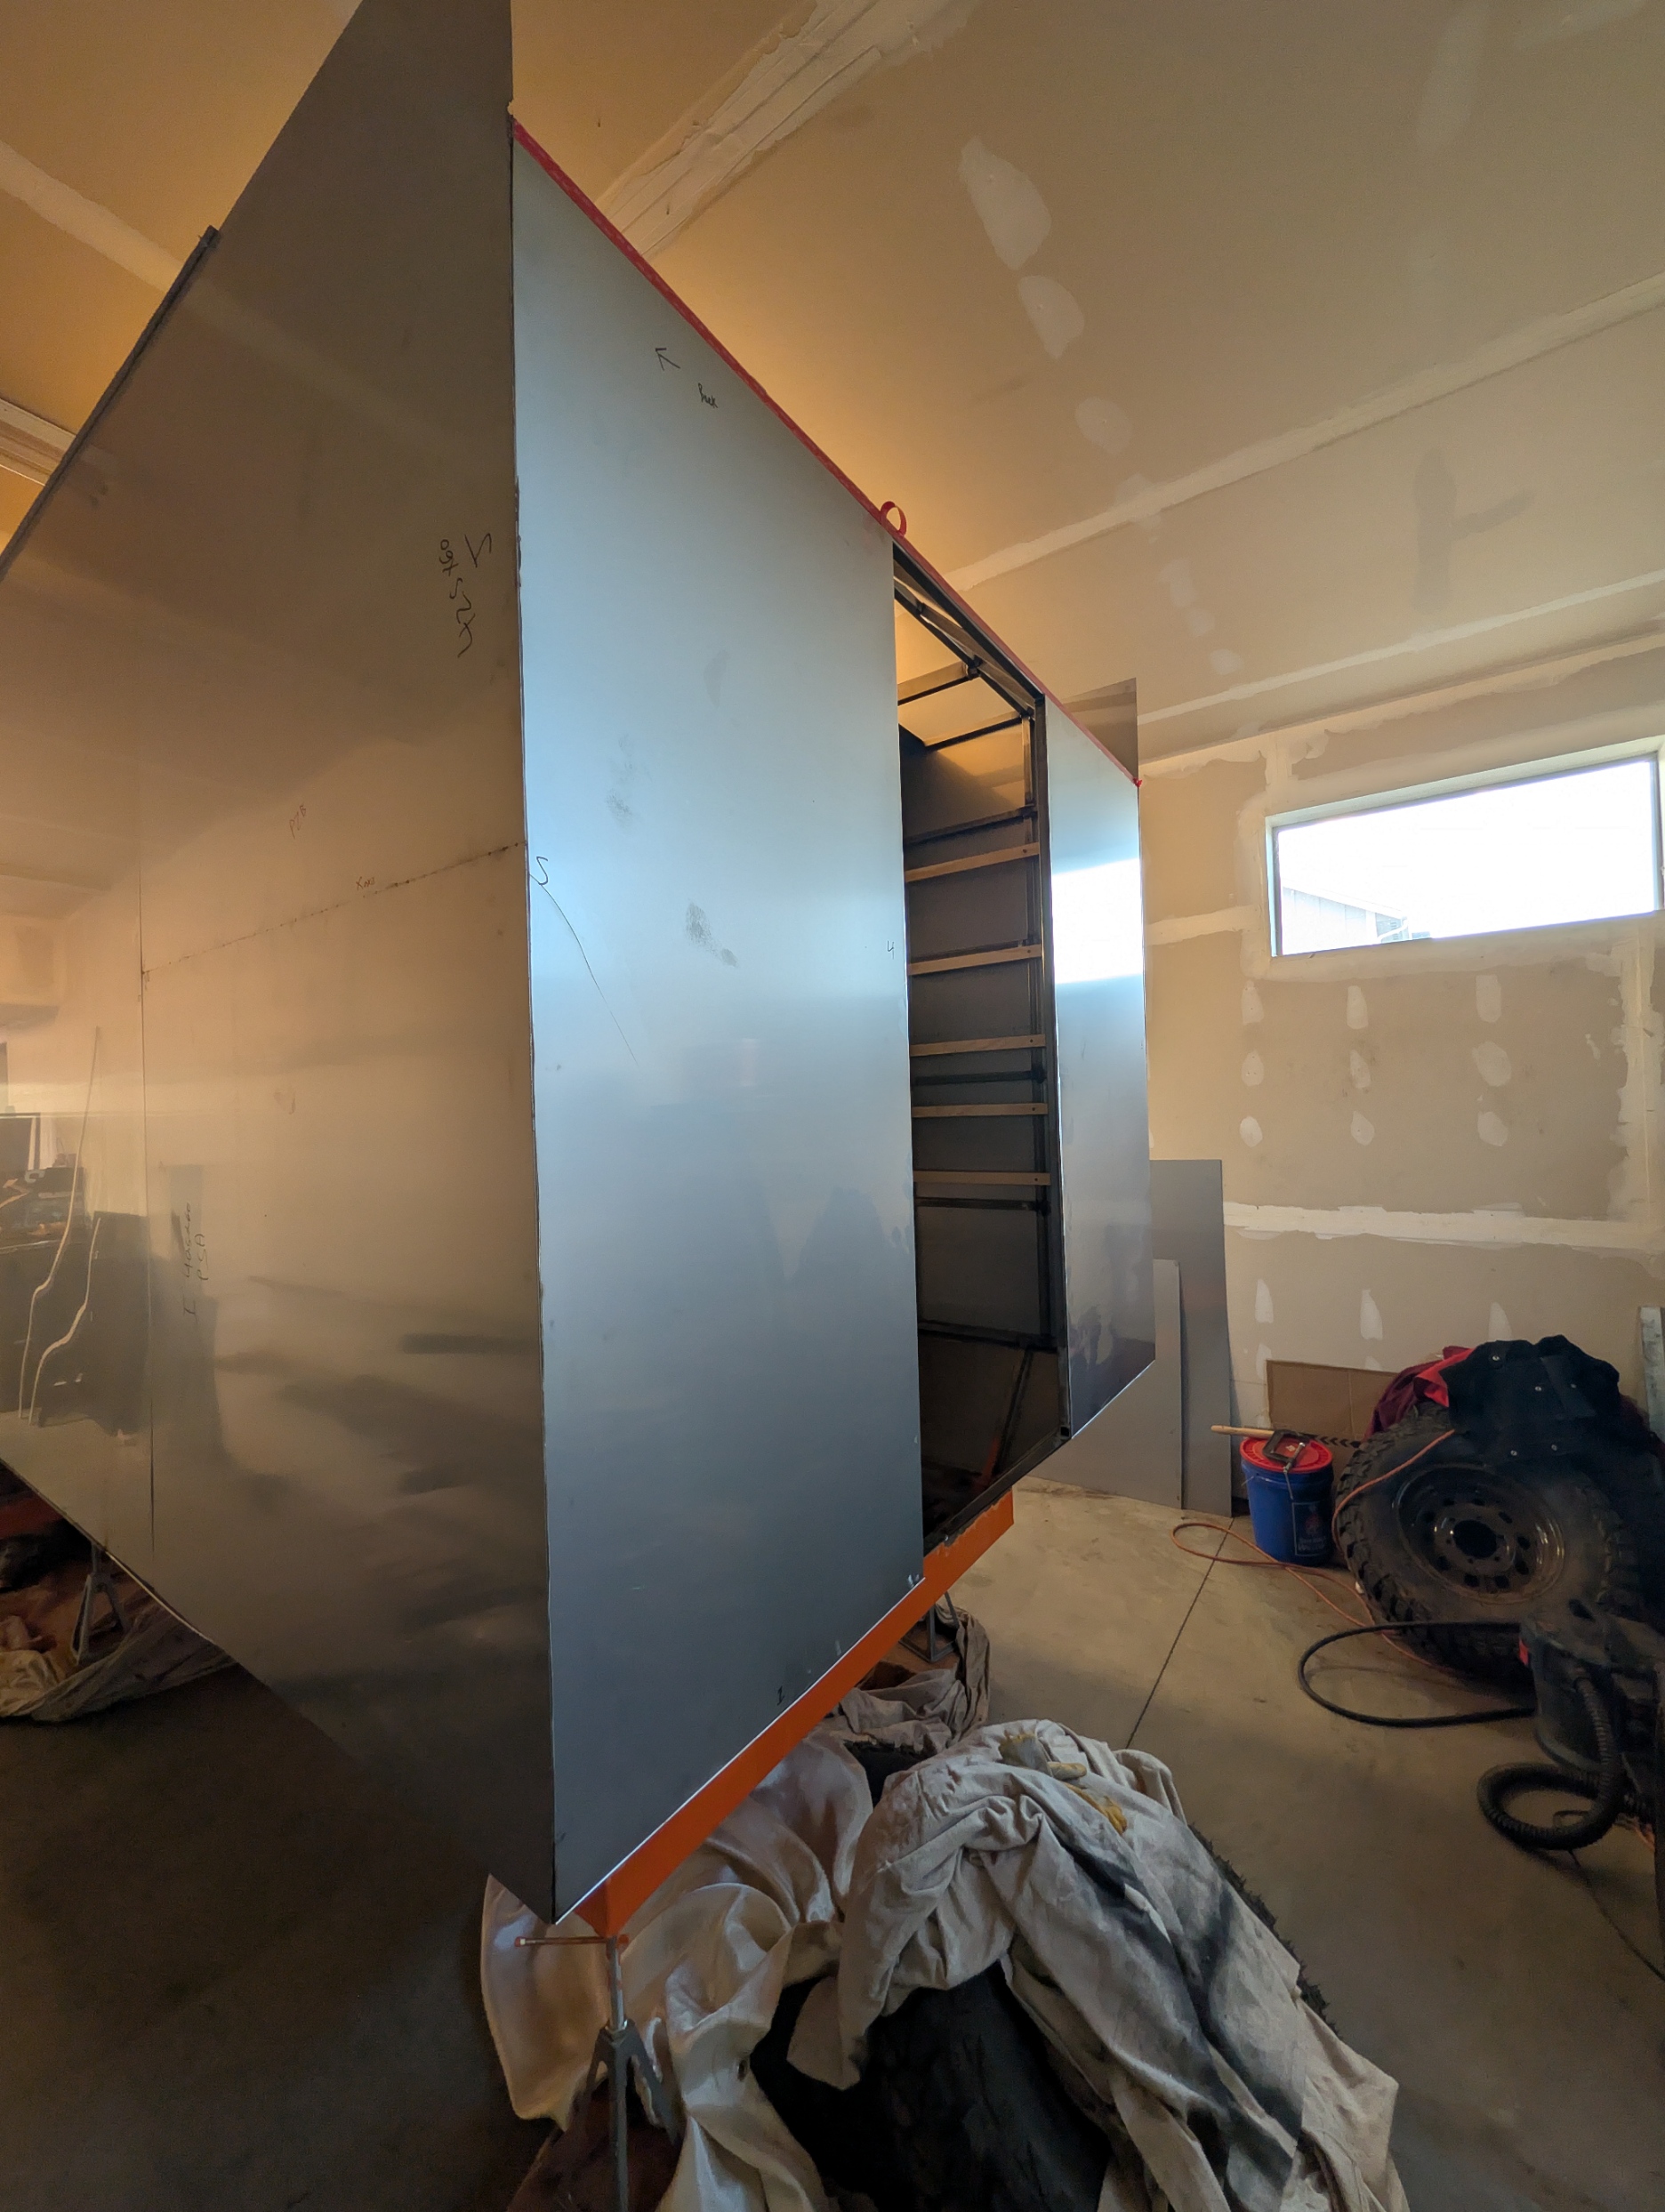
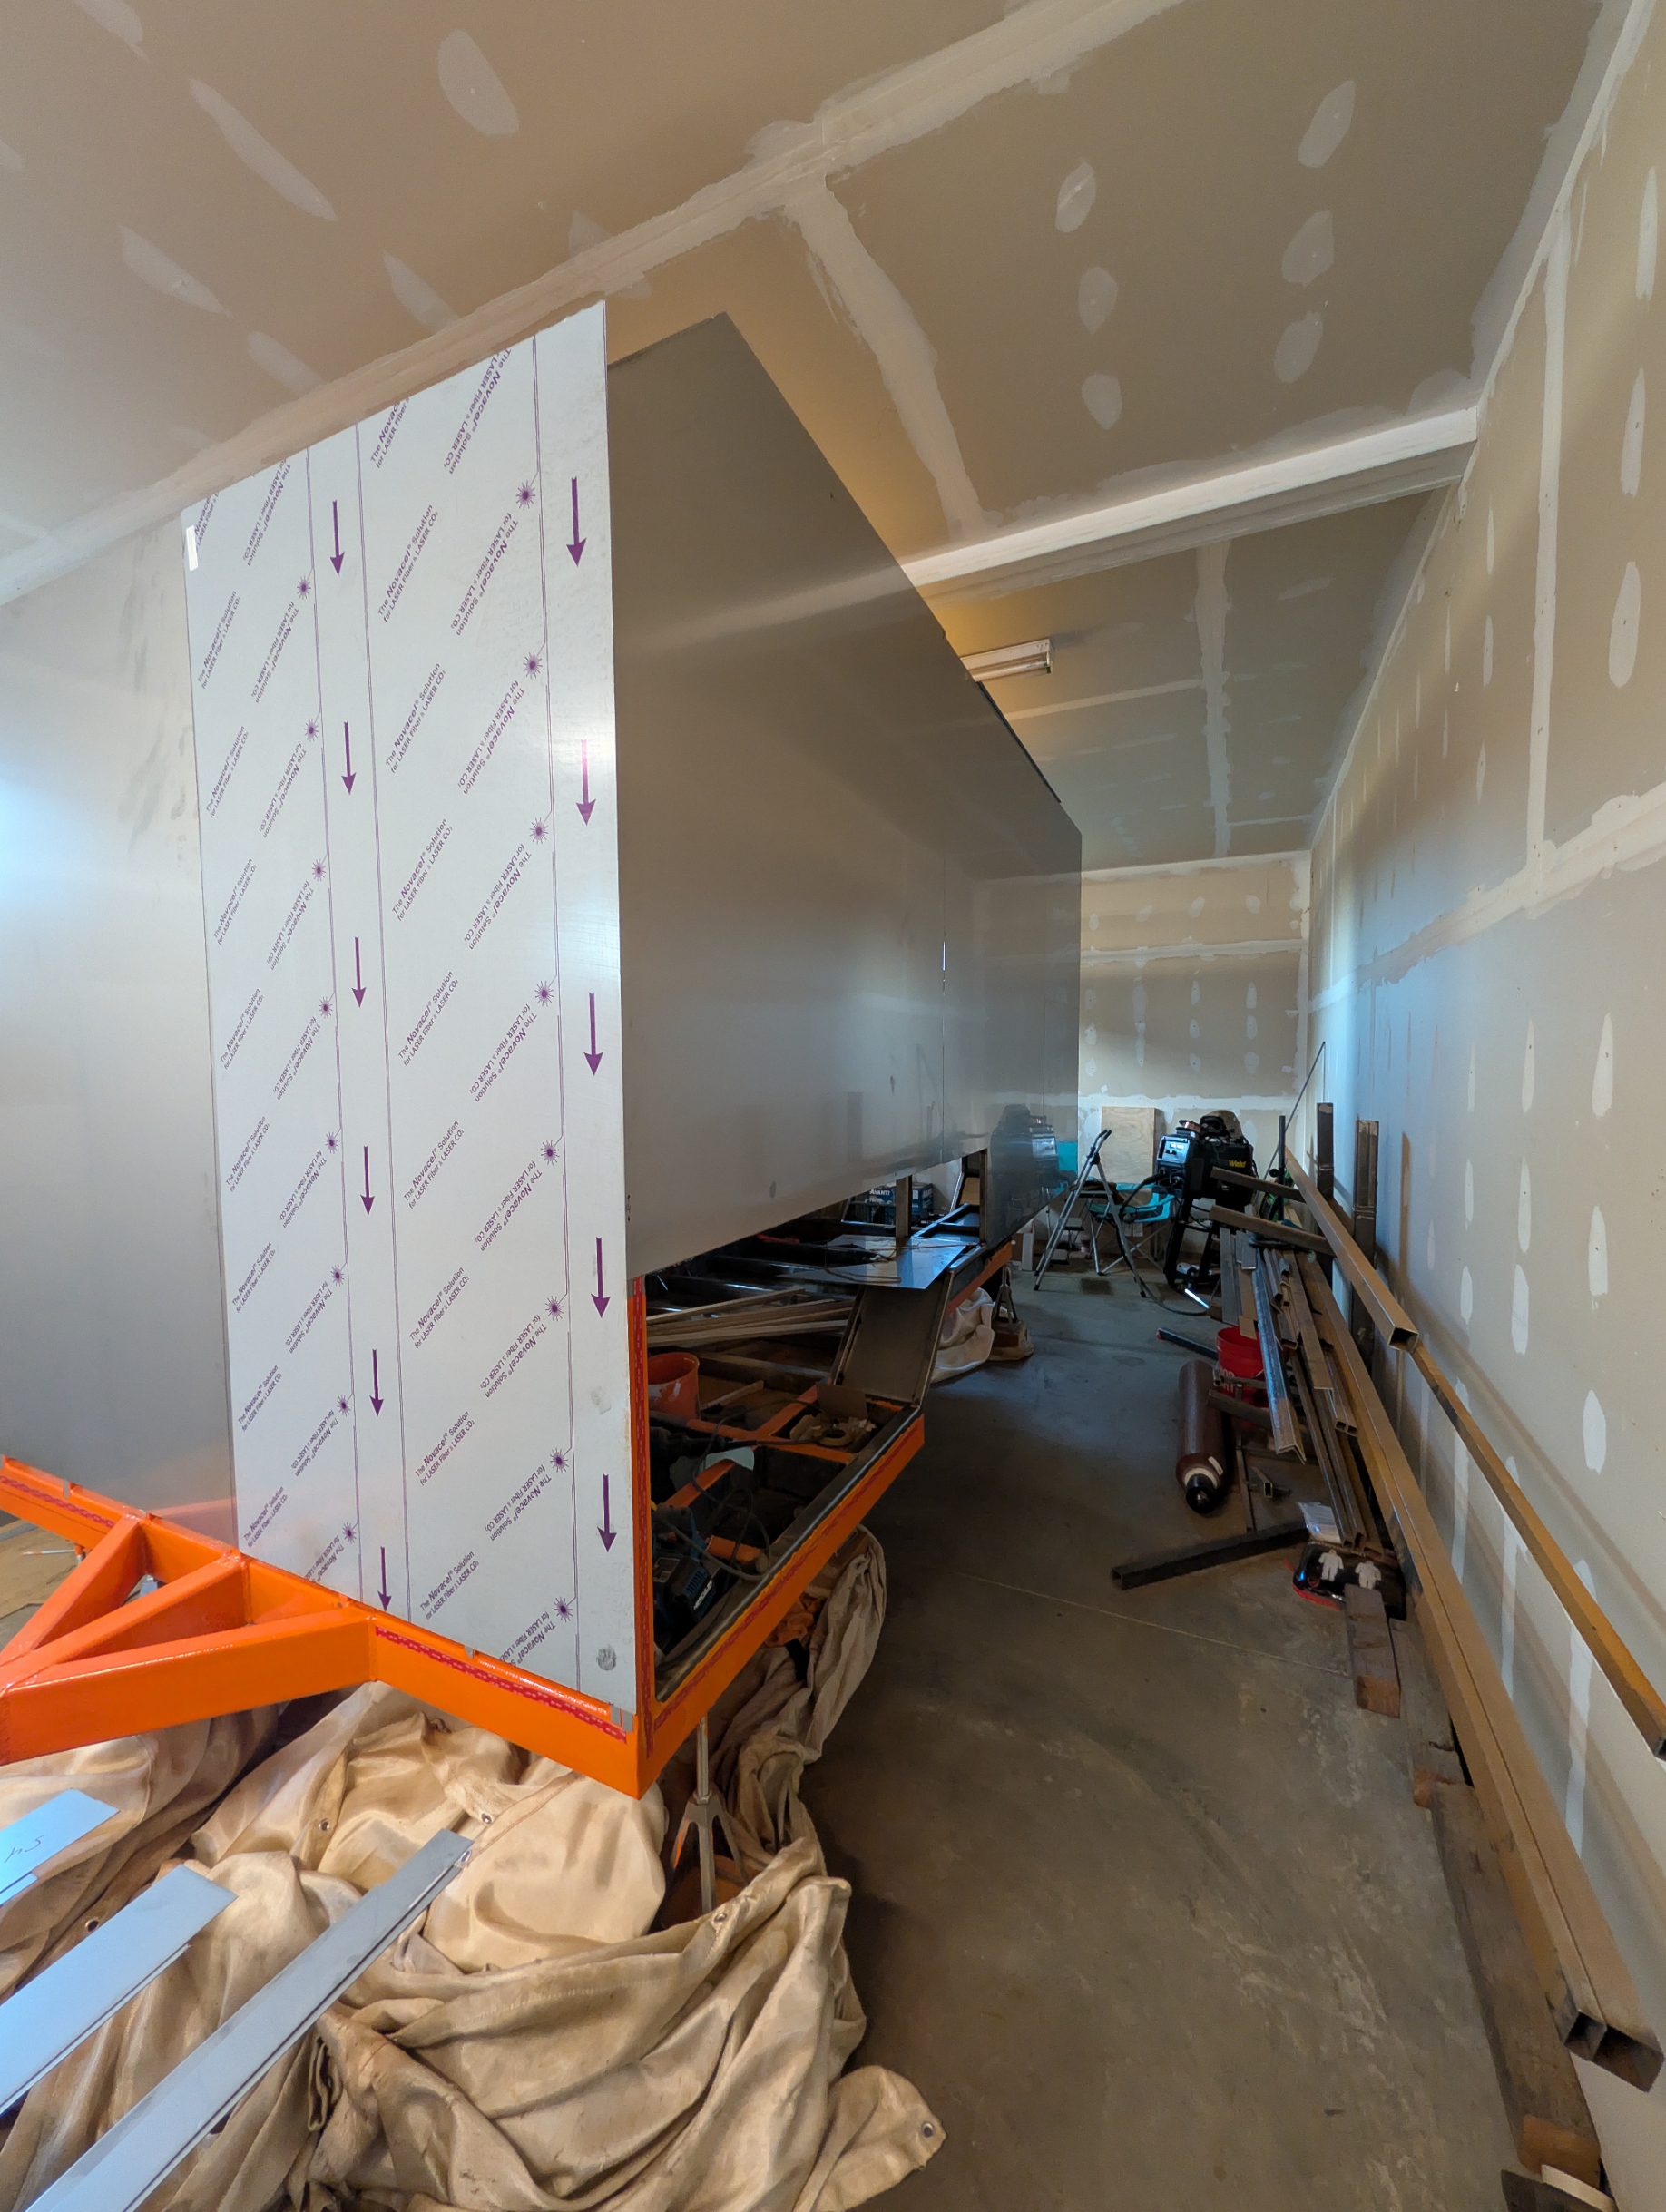
It's been awhile but I've been busy! There's a bit of a rush to get the camper out of the garage I'm renting, and I'm slipping past deadlines but oh well. I'm learning the better way to do things usually after I've spent a ton of time doing it the more difficult way, oh well! Since the last update I've gotten most™ of the siding on! While putting on the large panels I decided it was too difficult to get the gaps perfect for laser welding the 20ga stainless sheets so I decided to make trim pieces.
In my head it was "oh just a few edges, the siding panel seams, easy right?! HAHAAHAH no. I added it up and have over 28 different edges between all the weird angles I have. And even though some sheets I was able to fit up nicely if only some seams have a trim piece and others don't that'd look pretty strange so trim for everything!
However a huge issue I discovered is my Evolution cold cut circular saw with a stainless blade wears the $60 blade out VERY quickly, like in 15-20 feet of cutting quickly. Which is not going to fly with hundreds of feet of cuts between the lower fender/wheel well pieces, and everything else. It DOES give VERY accurate cuts however when a straight edge is used but oh well. That lead me to cut things out with cutting wheels and an angle grinder for a bit, which worked OK, not super accurate, lots of cleanup and deburring and not very fast. Then I tried a regular circular saw with an abrasive cutoff wheel and a straight edge which was more accurate but slow, a ton of dust, debris, and still required a lot of cleanup, not to mention I couldn't find thin kerf cutting blades for the circular saw on short notice so I was back to the angle grinder.
Then I thought of the laser welder has a cutting function. After some investigation it would barely cut 20ga stainless which wasn't right. When I hooked it up to compressed air at 80psi instead of argon it cut up to 1/8" but had a lot of dross and oxidation. Not to mention I really needed an oil-less air compressor or an expensive heavy duty oil and moisture separator so the laser's optics which are partly cooled by the shielding gas flow don't get oil residue or moisture on them.
I needed an inert gas to cut with and I already had a cylinder of argon for welding, but welding regulators only supply fairly low pressure which is fixed and the flow rate can be adjusted. Cutting works best between 80-100 psi and after some troubleshooting a nitrogen regulator used in HVAC work would work with my argon tank, I just had to make sure I don't overpressure the laser welder as the new regulator would go up to 800 PSI output and the laser welder has a maximum of less than 140. Cutting with nitrogen works too but I didn't want to buy a nitrogen tank ($320) for maybe a tank to a tank and a half of argon ($63/fill) of cutting. If I was cutting more or was going to get into CNC cutting stainless then I'd go the nitrogen route.
ANYWAY, I finally get the cutting down and it goes quick! The handheld laser "torch" is not really setup for using a guide however the way the cutting tip is so my cuts aren't as consistent as I want but I got the job done. In hindsight I should've just had a shop use their industrial shear to cut the pieces I need. Since that can be very straight. But live and learn.
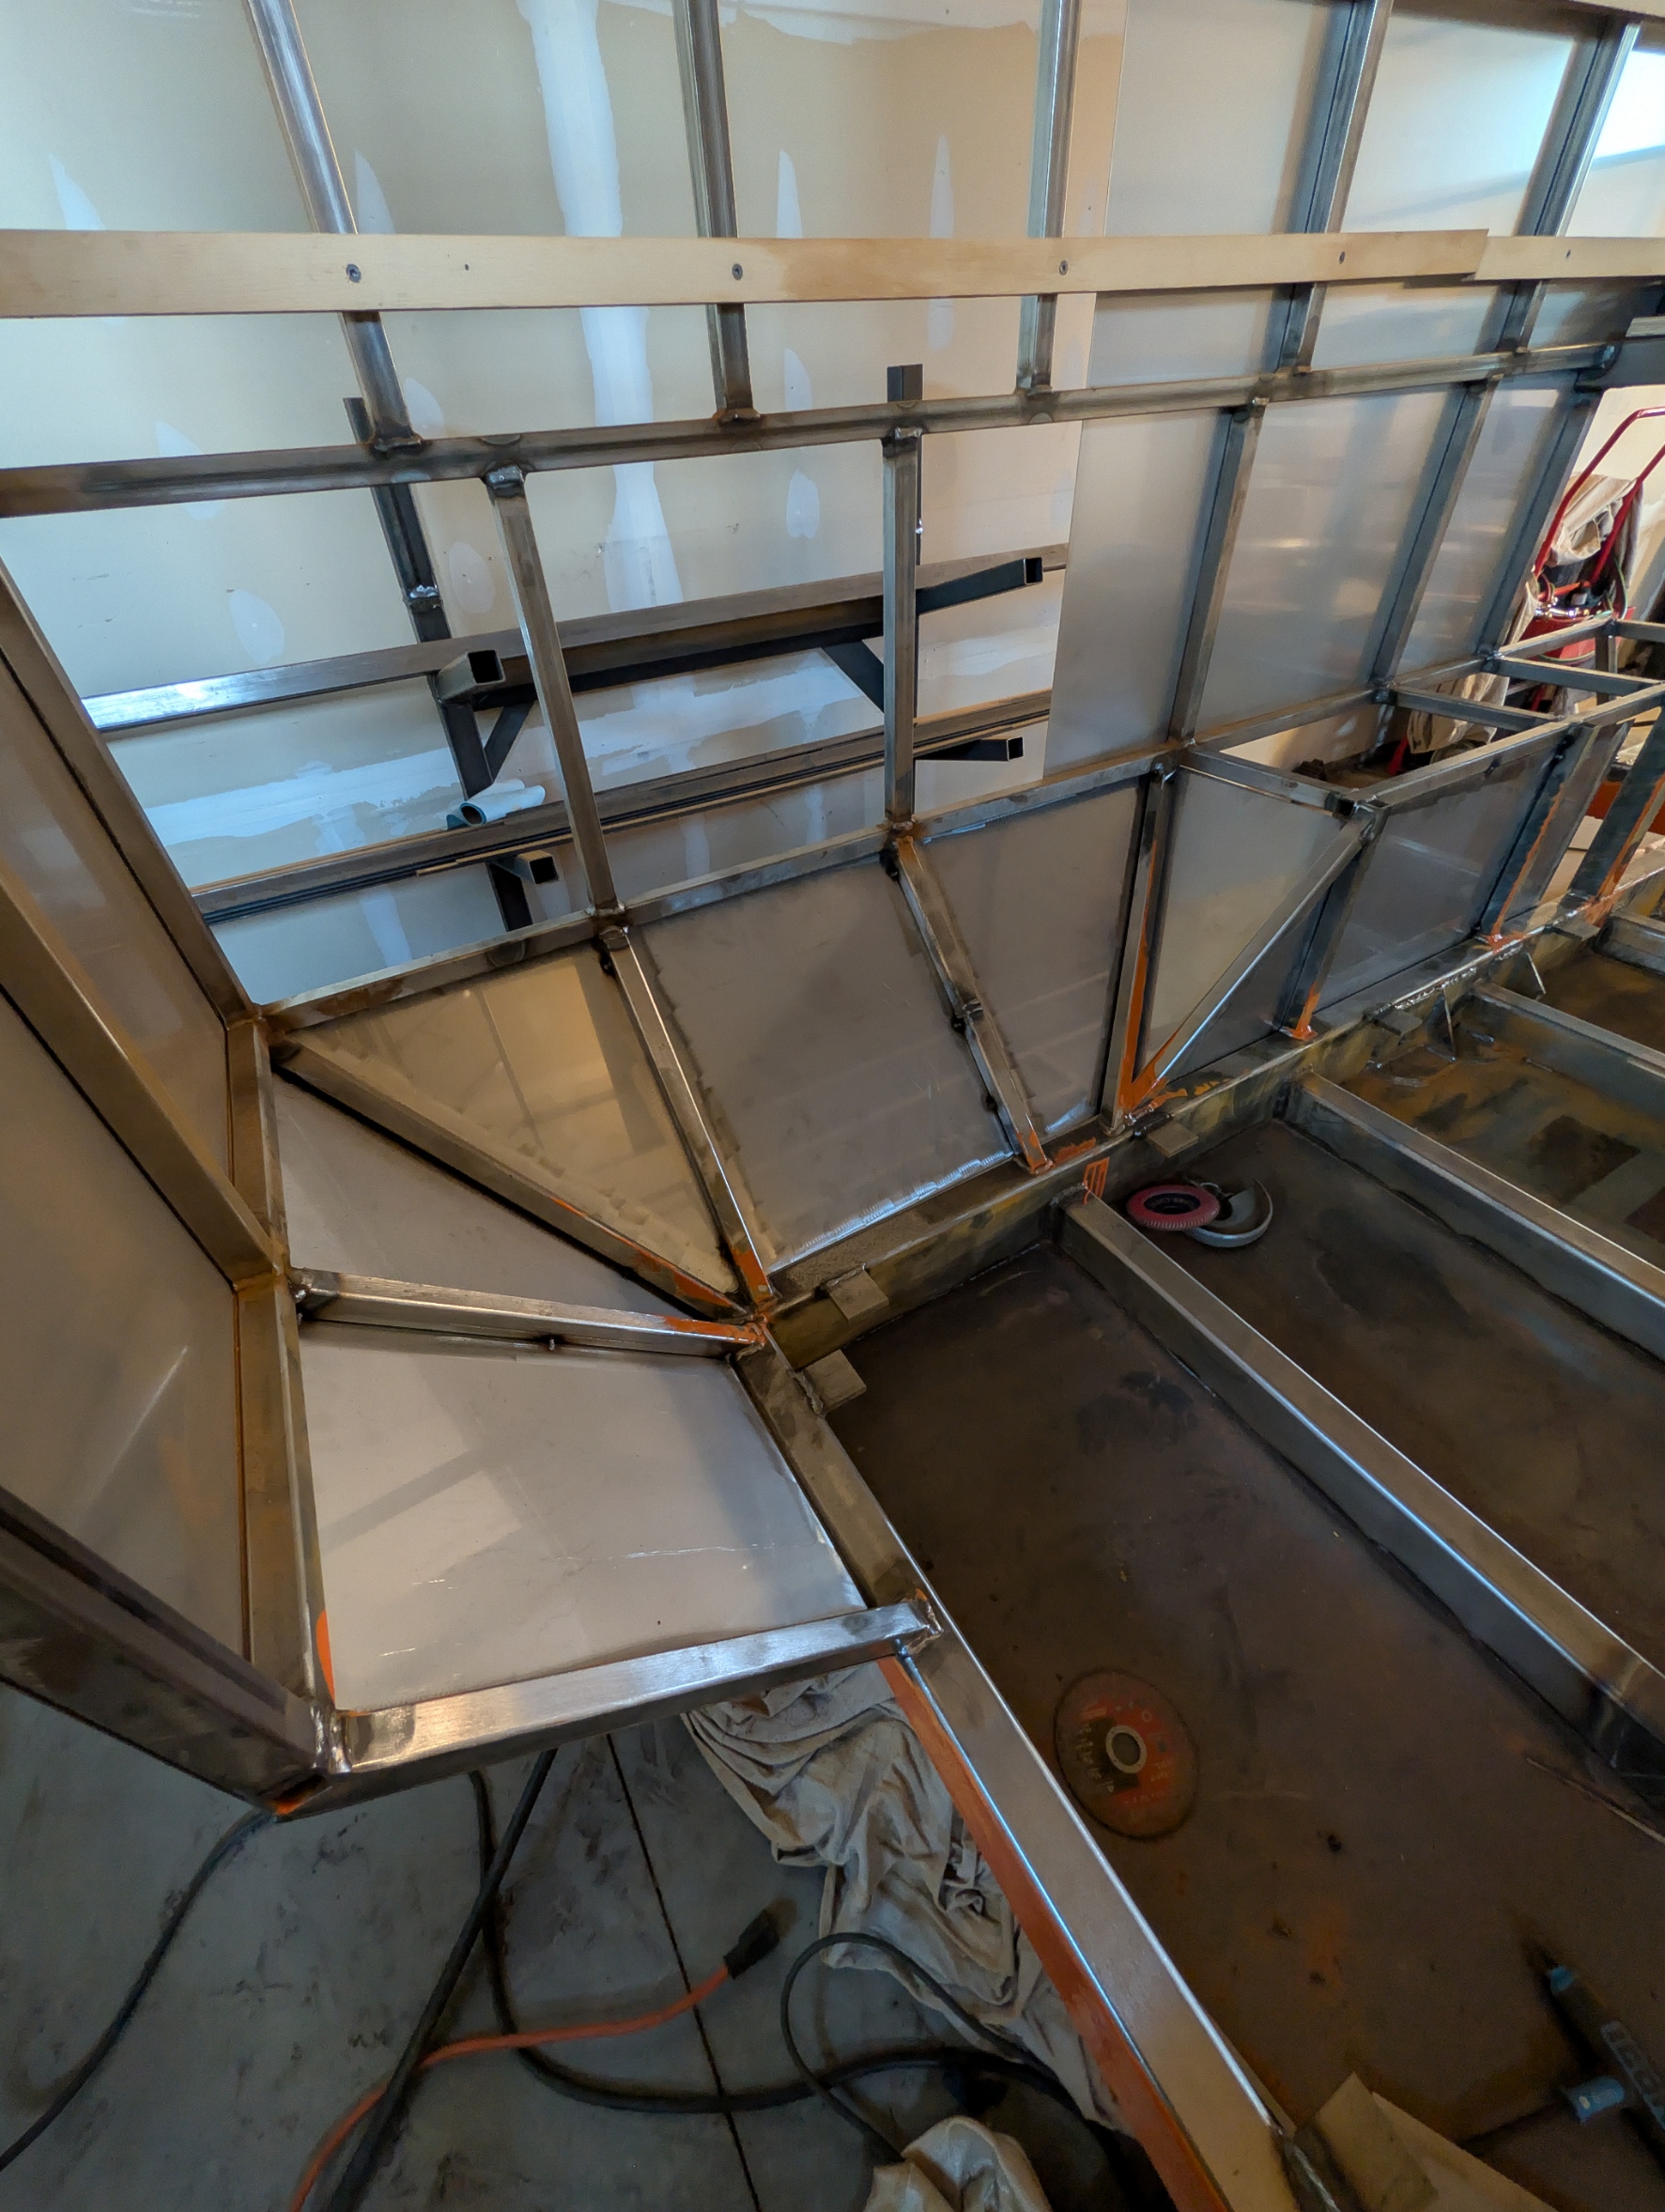
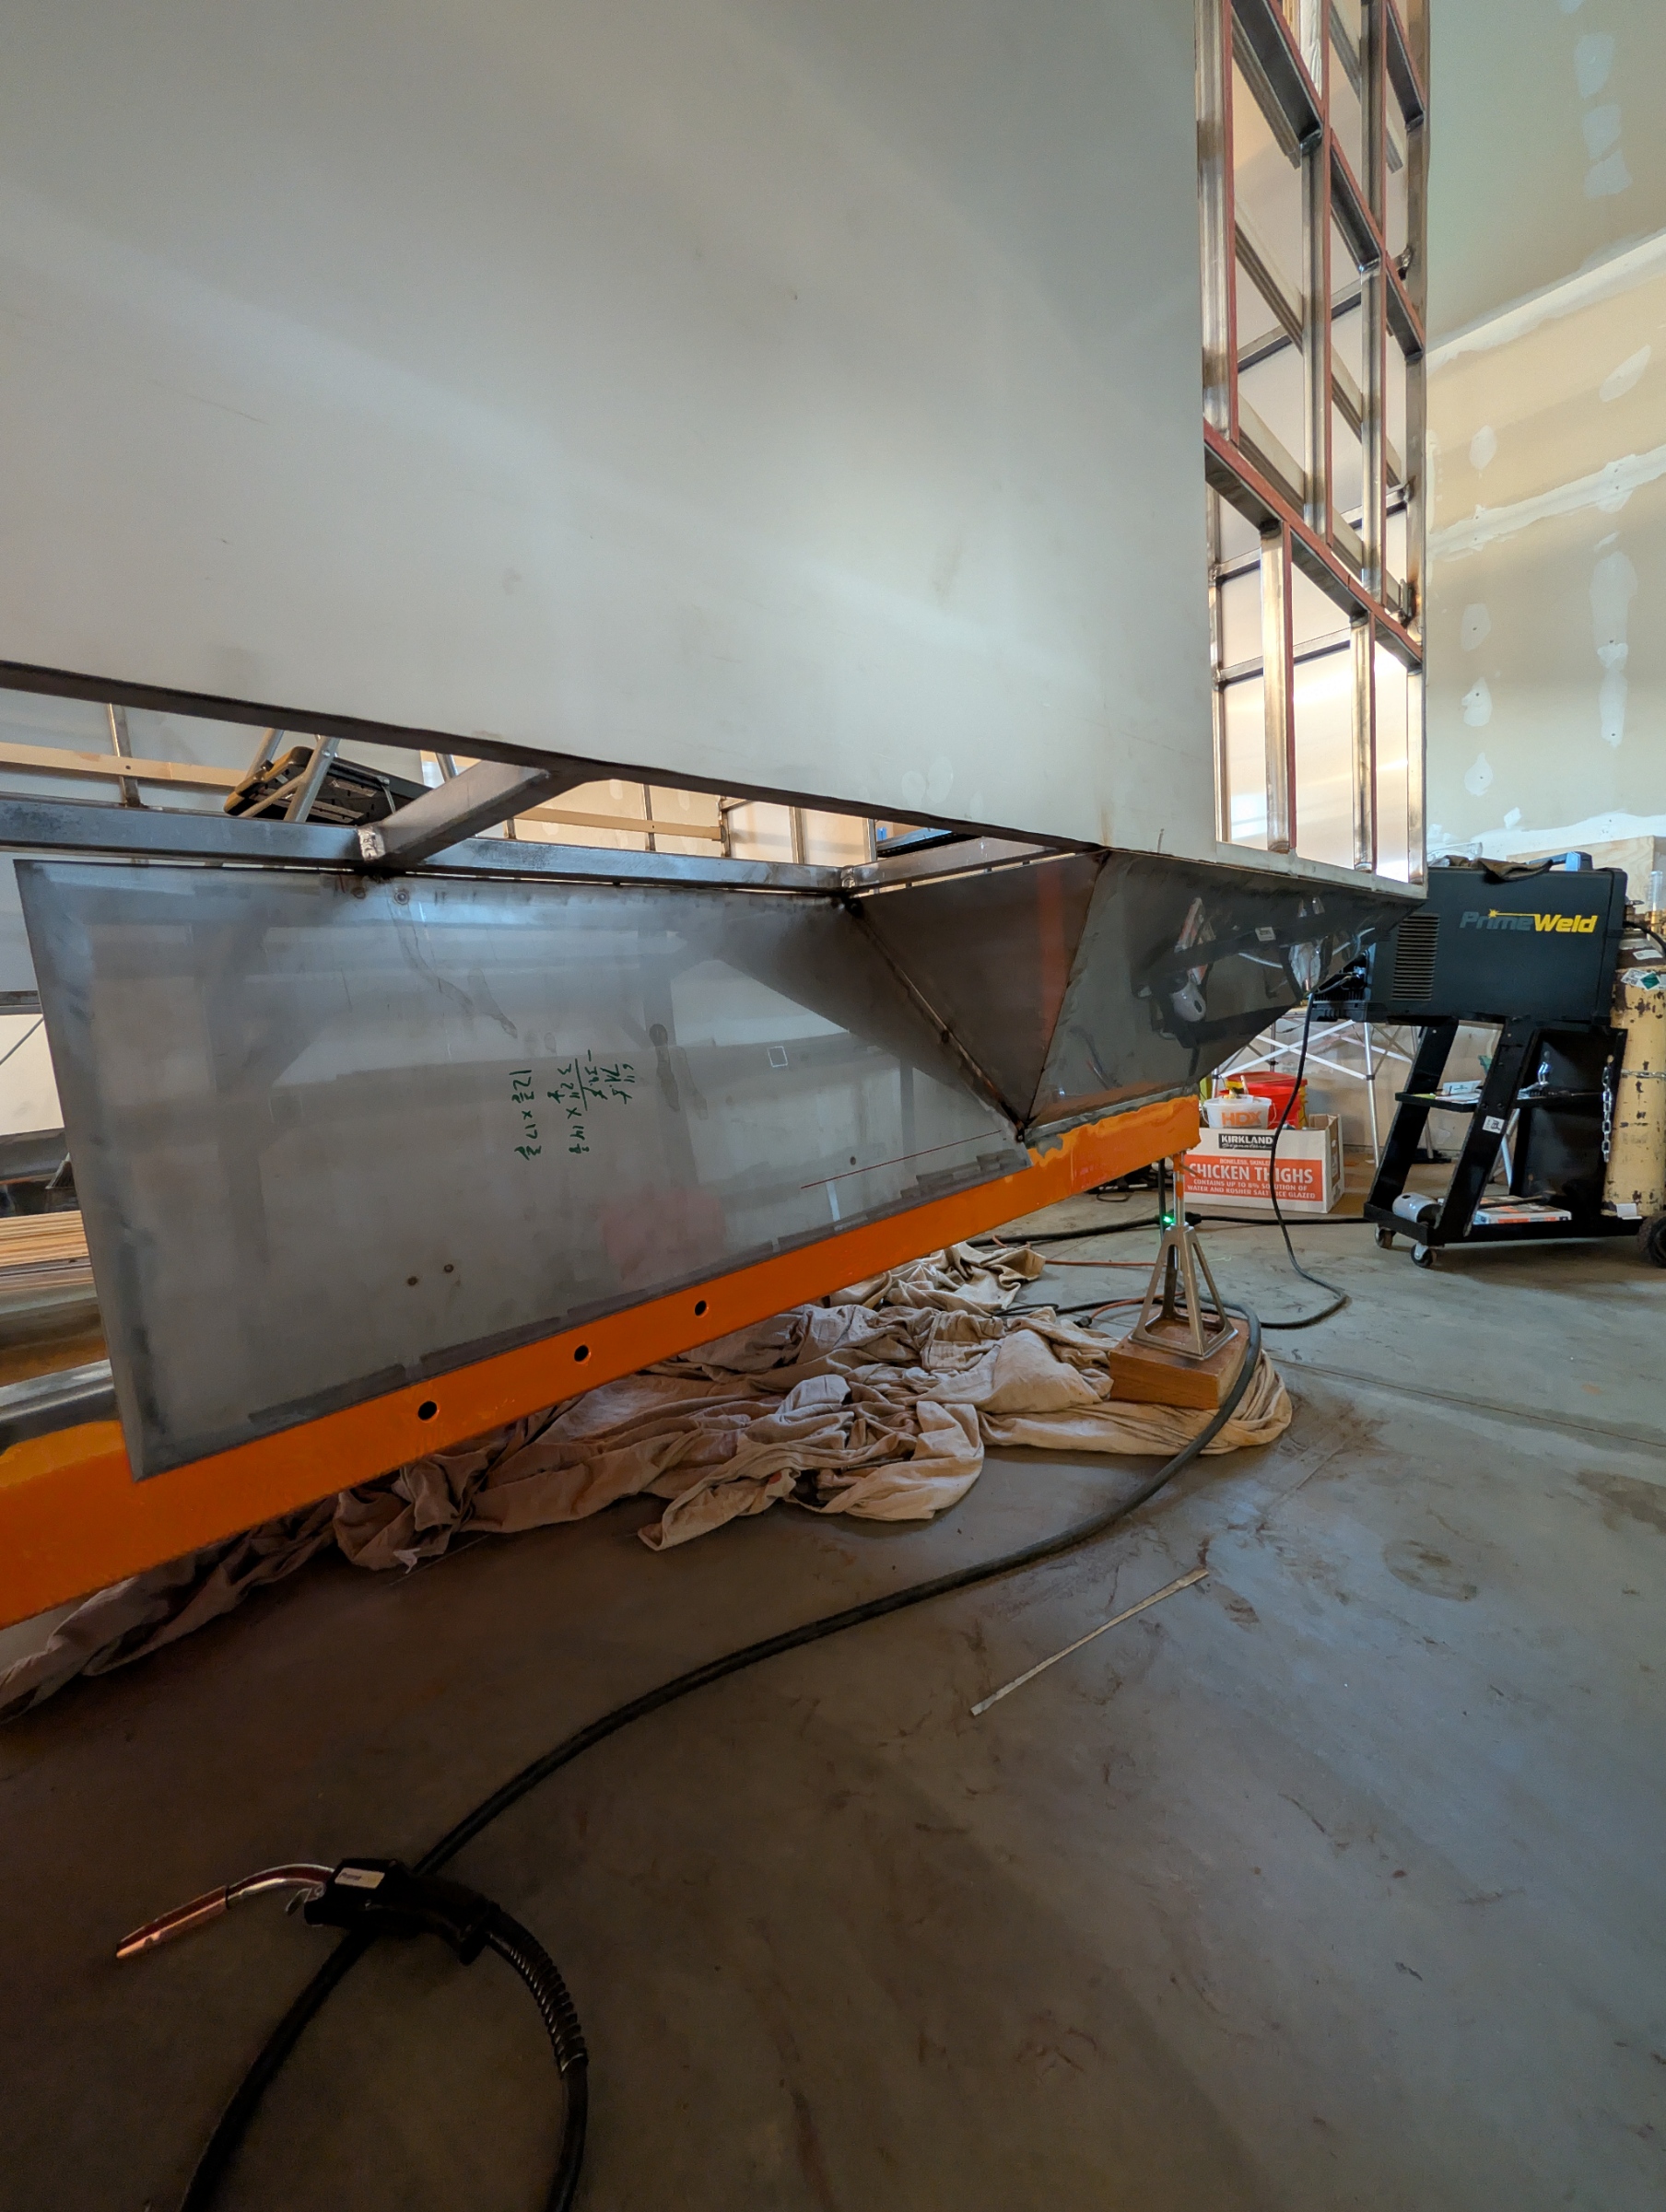
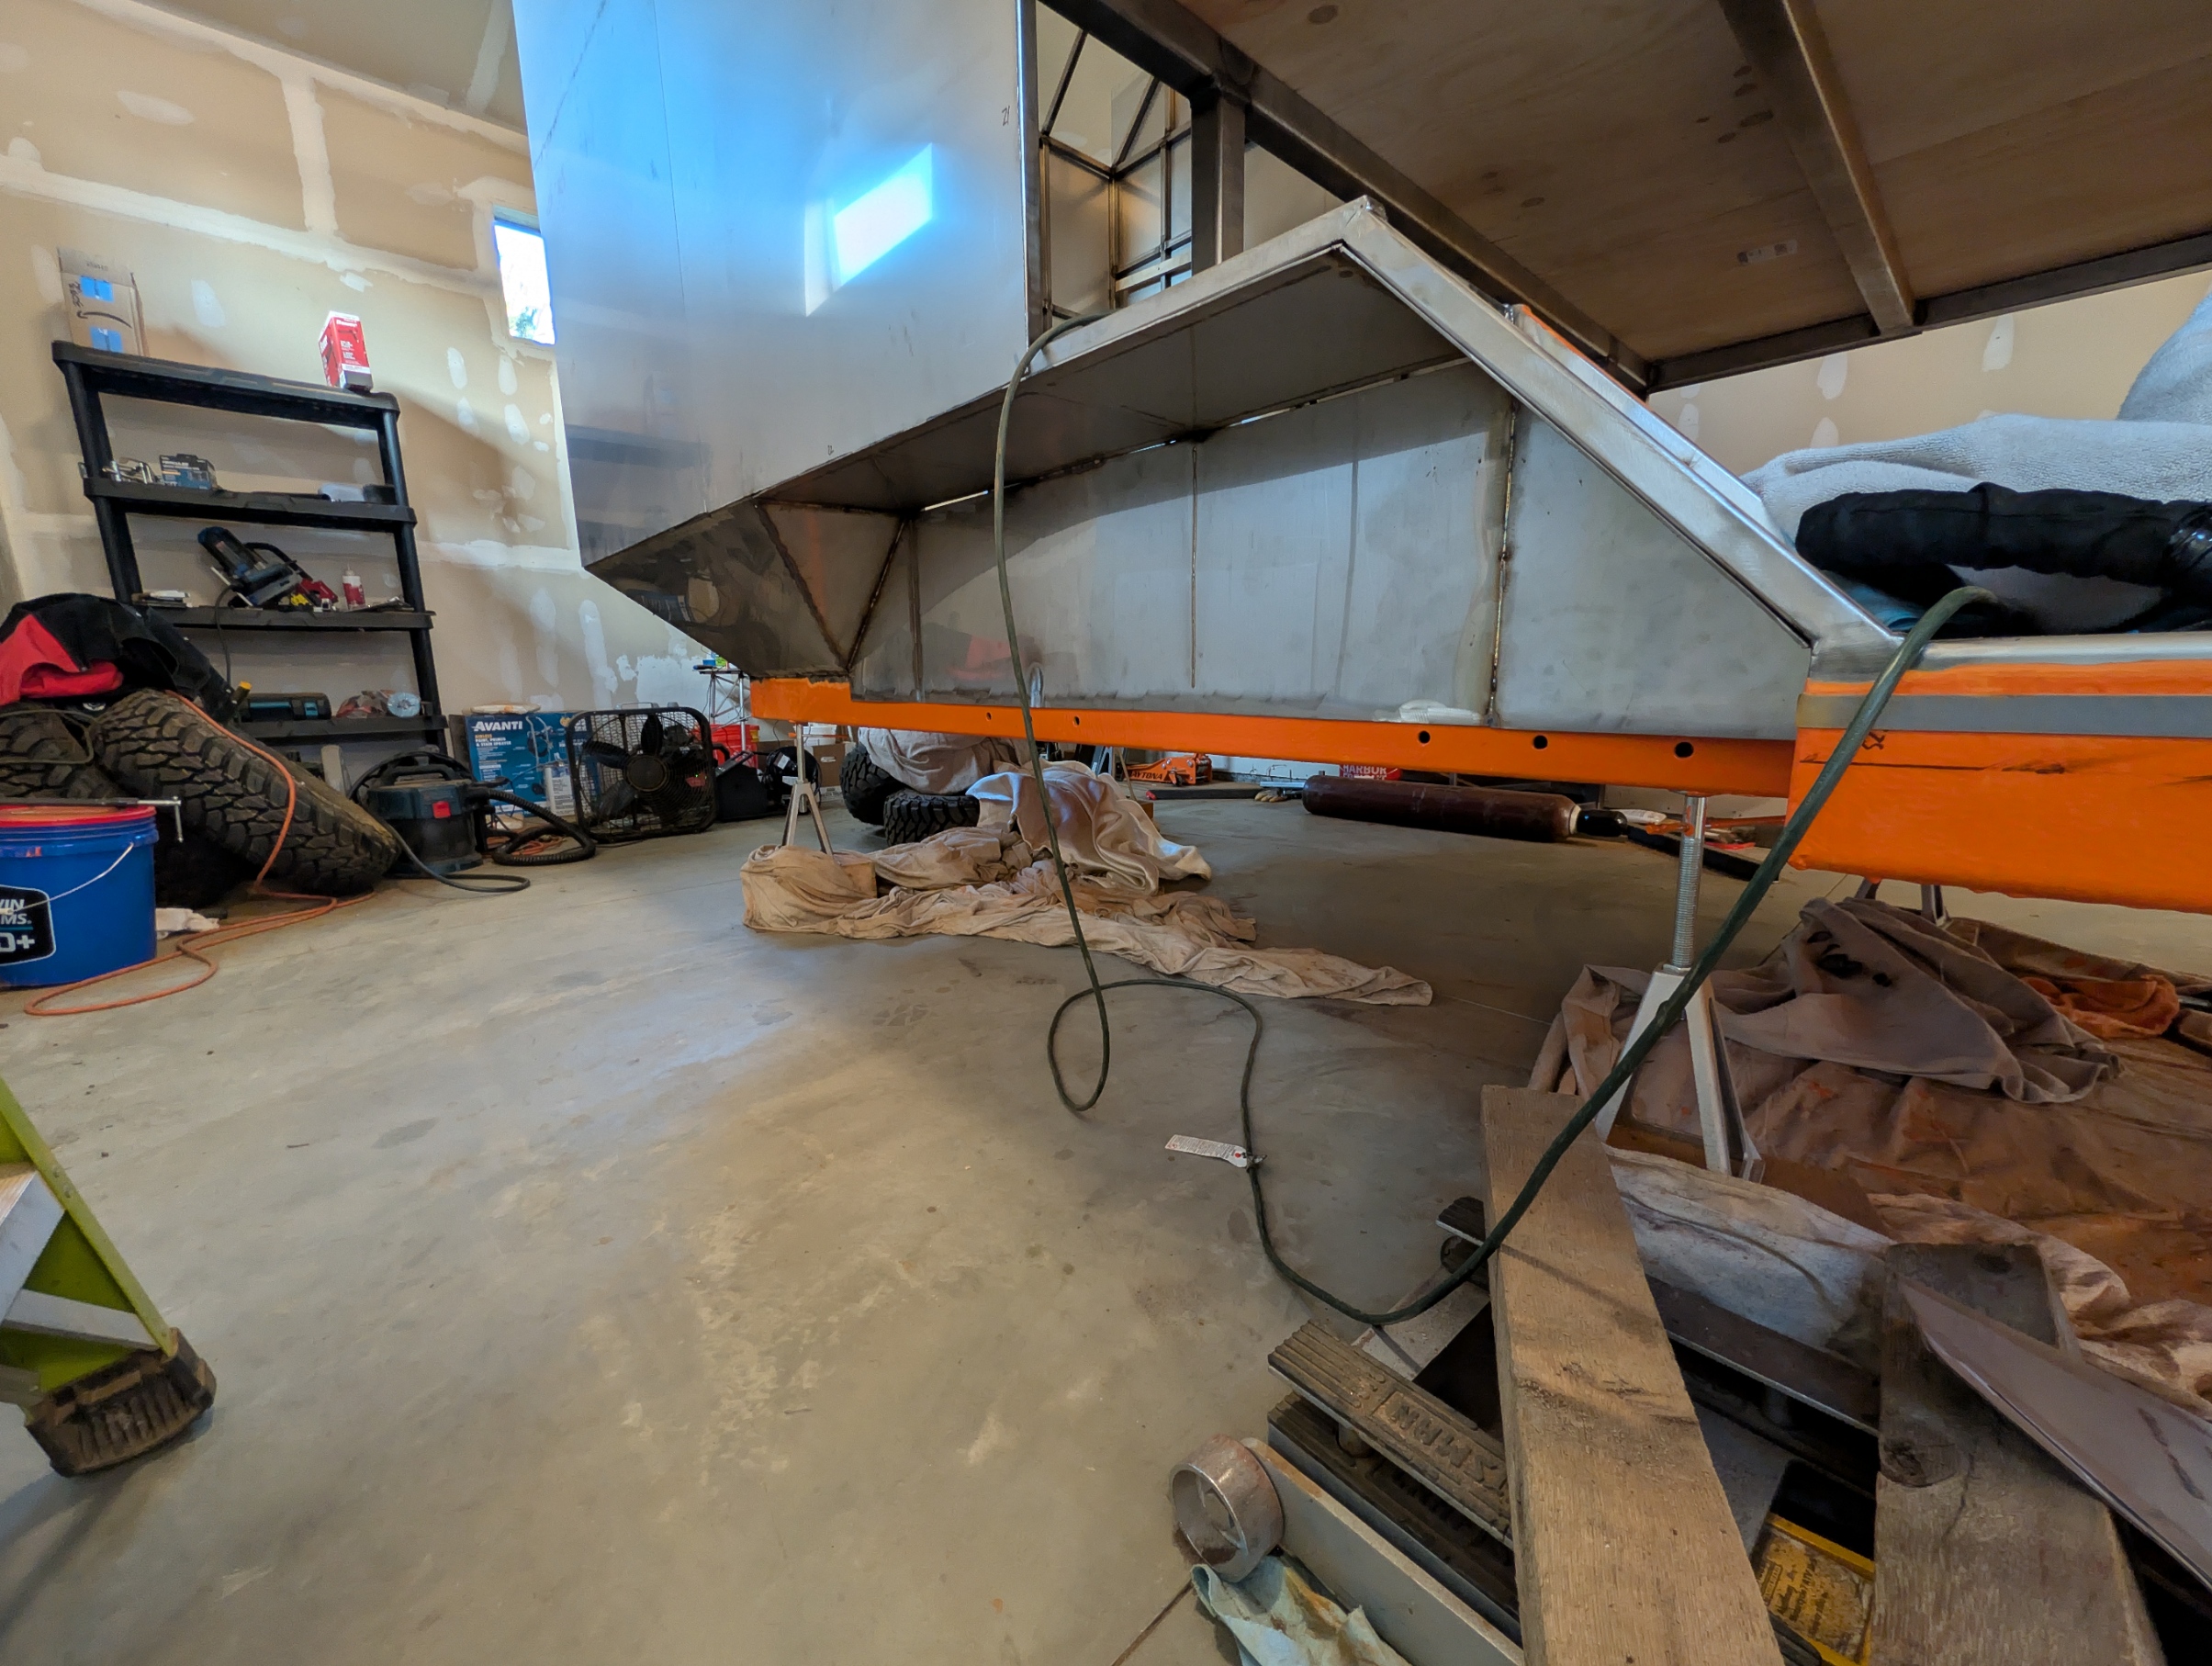
After much review and since the metal walls minor distortion from welding in them I decided for the 20ga siding and roof to attach it using VHB tape, which would help with sound deadening, thermal transfer, and adjust for some of the wall's local distortion. The 14ga thick lower fender/wheel wells I'd weld onto the carbon steel frame since it was a bit thicker and easier to do.
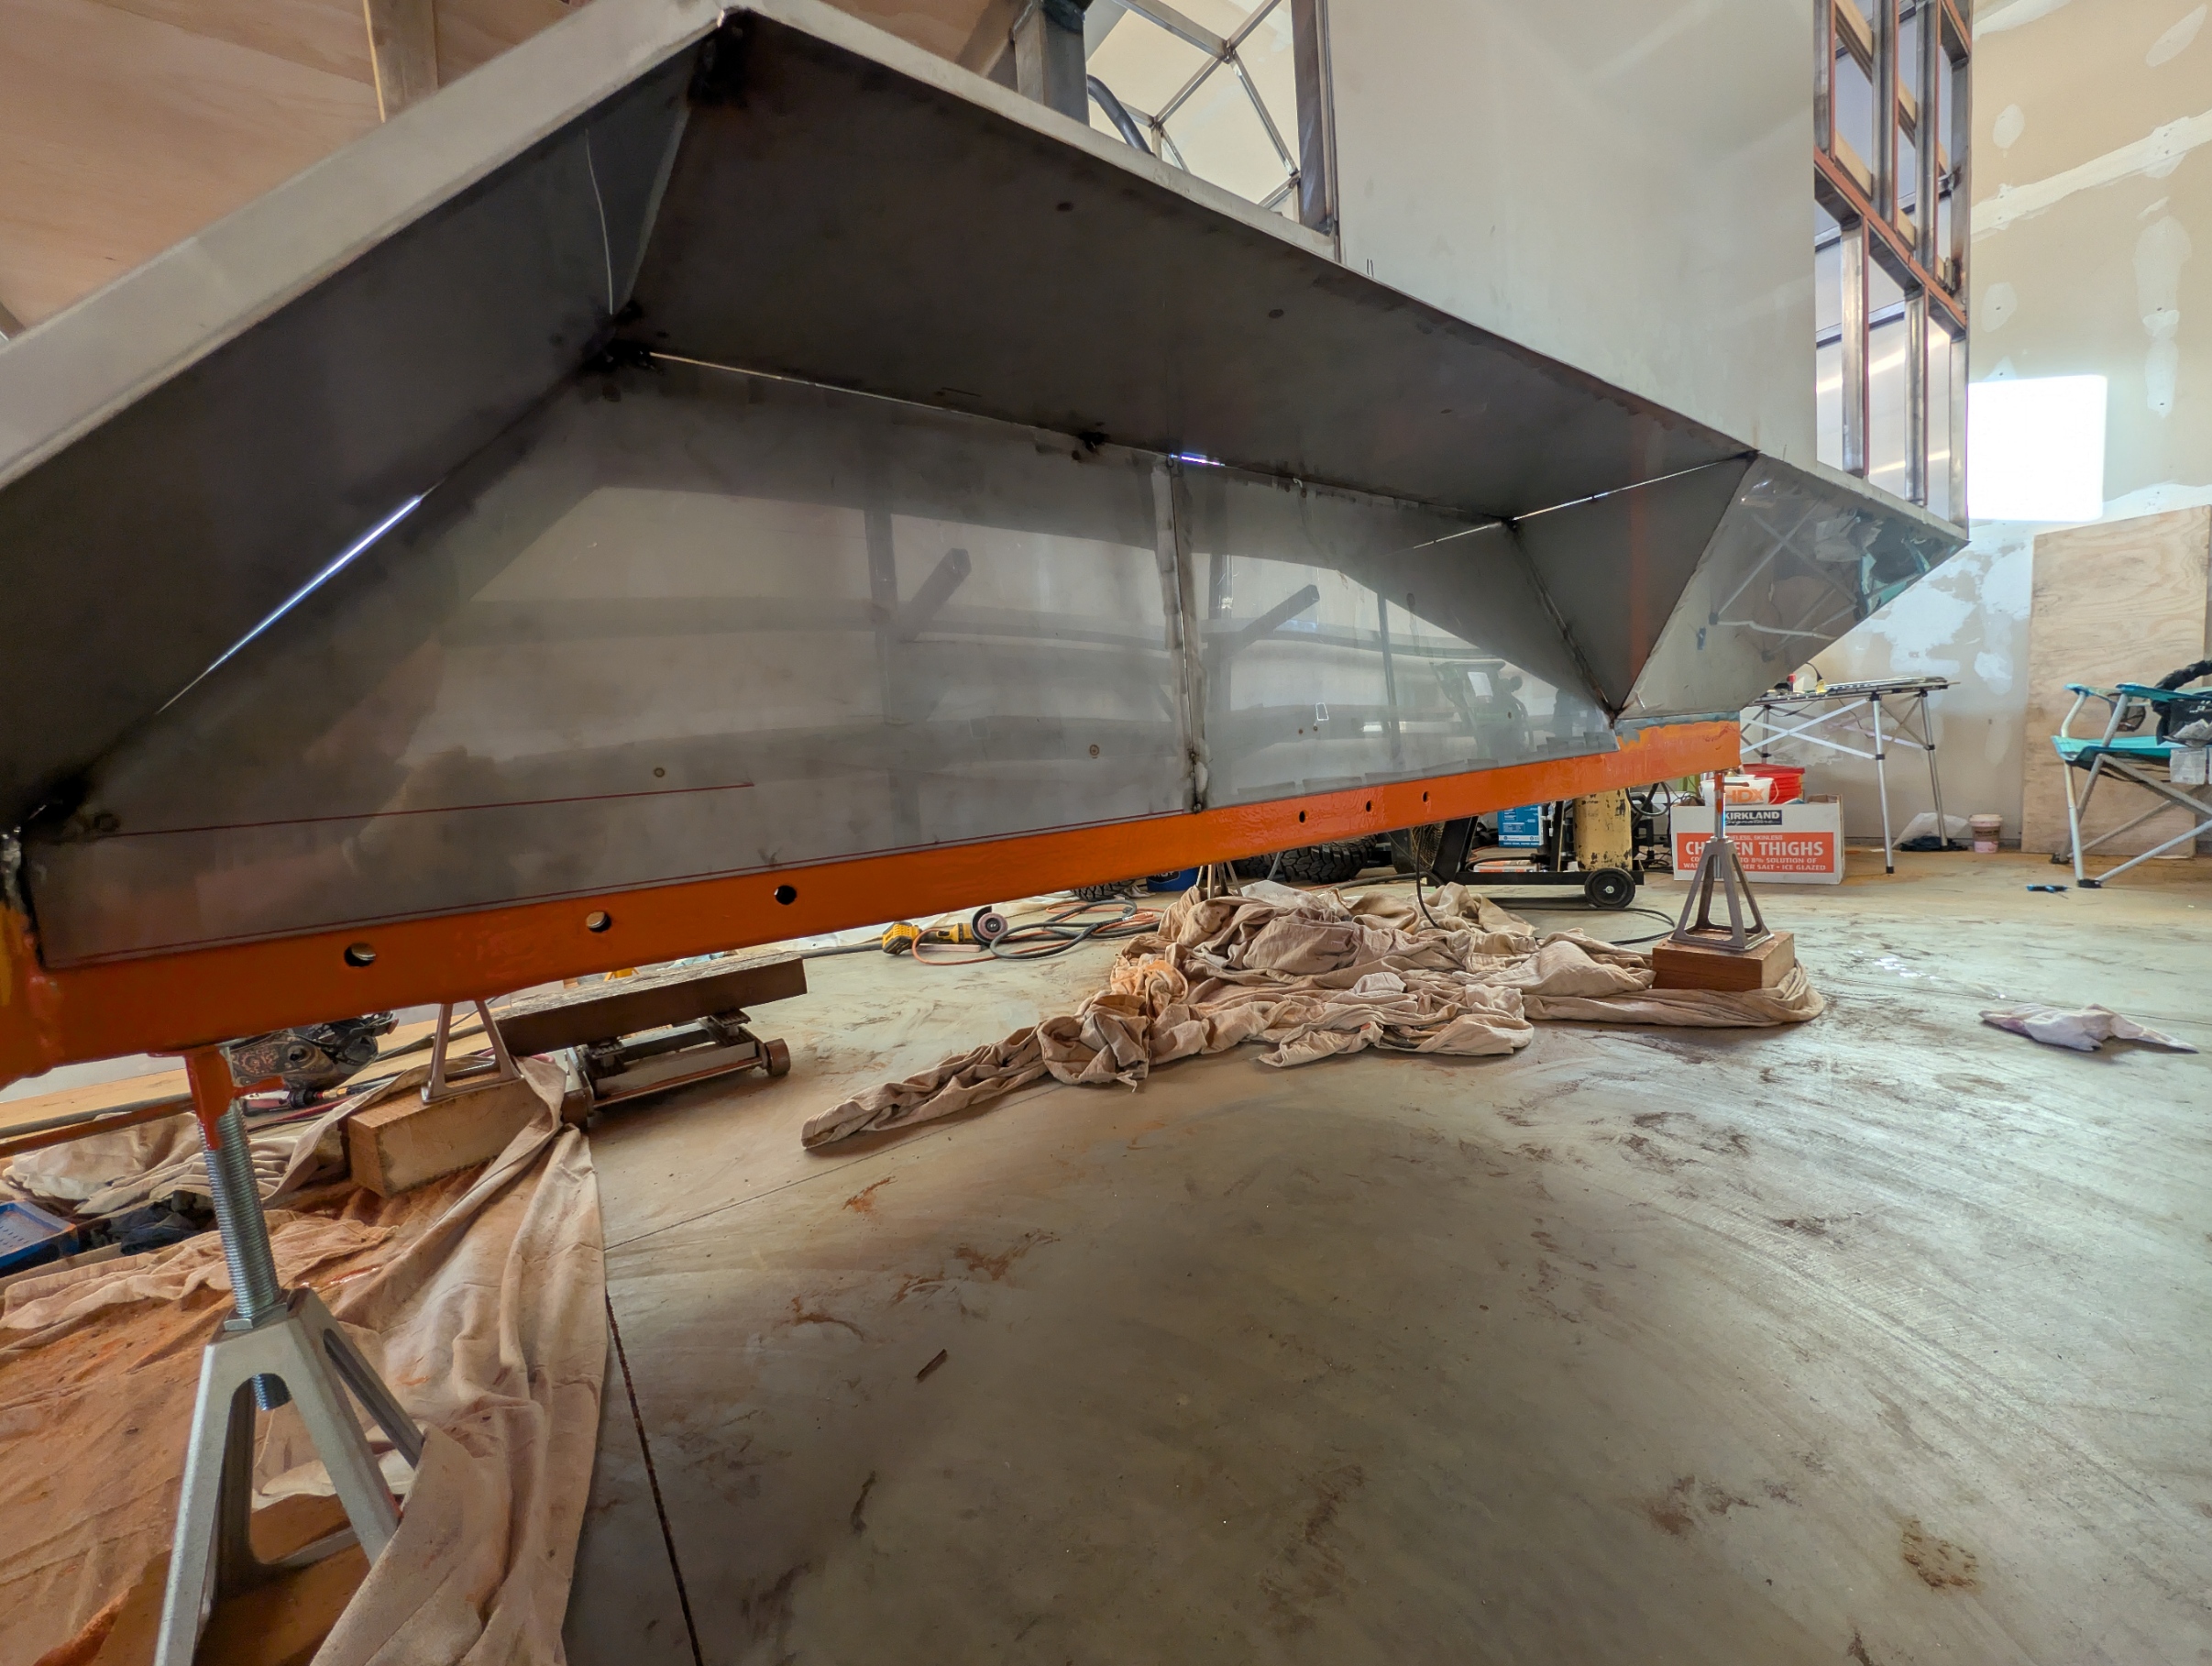
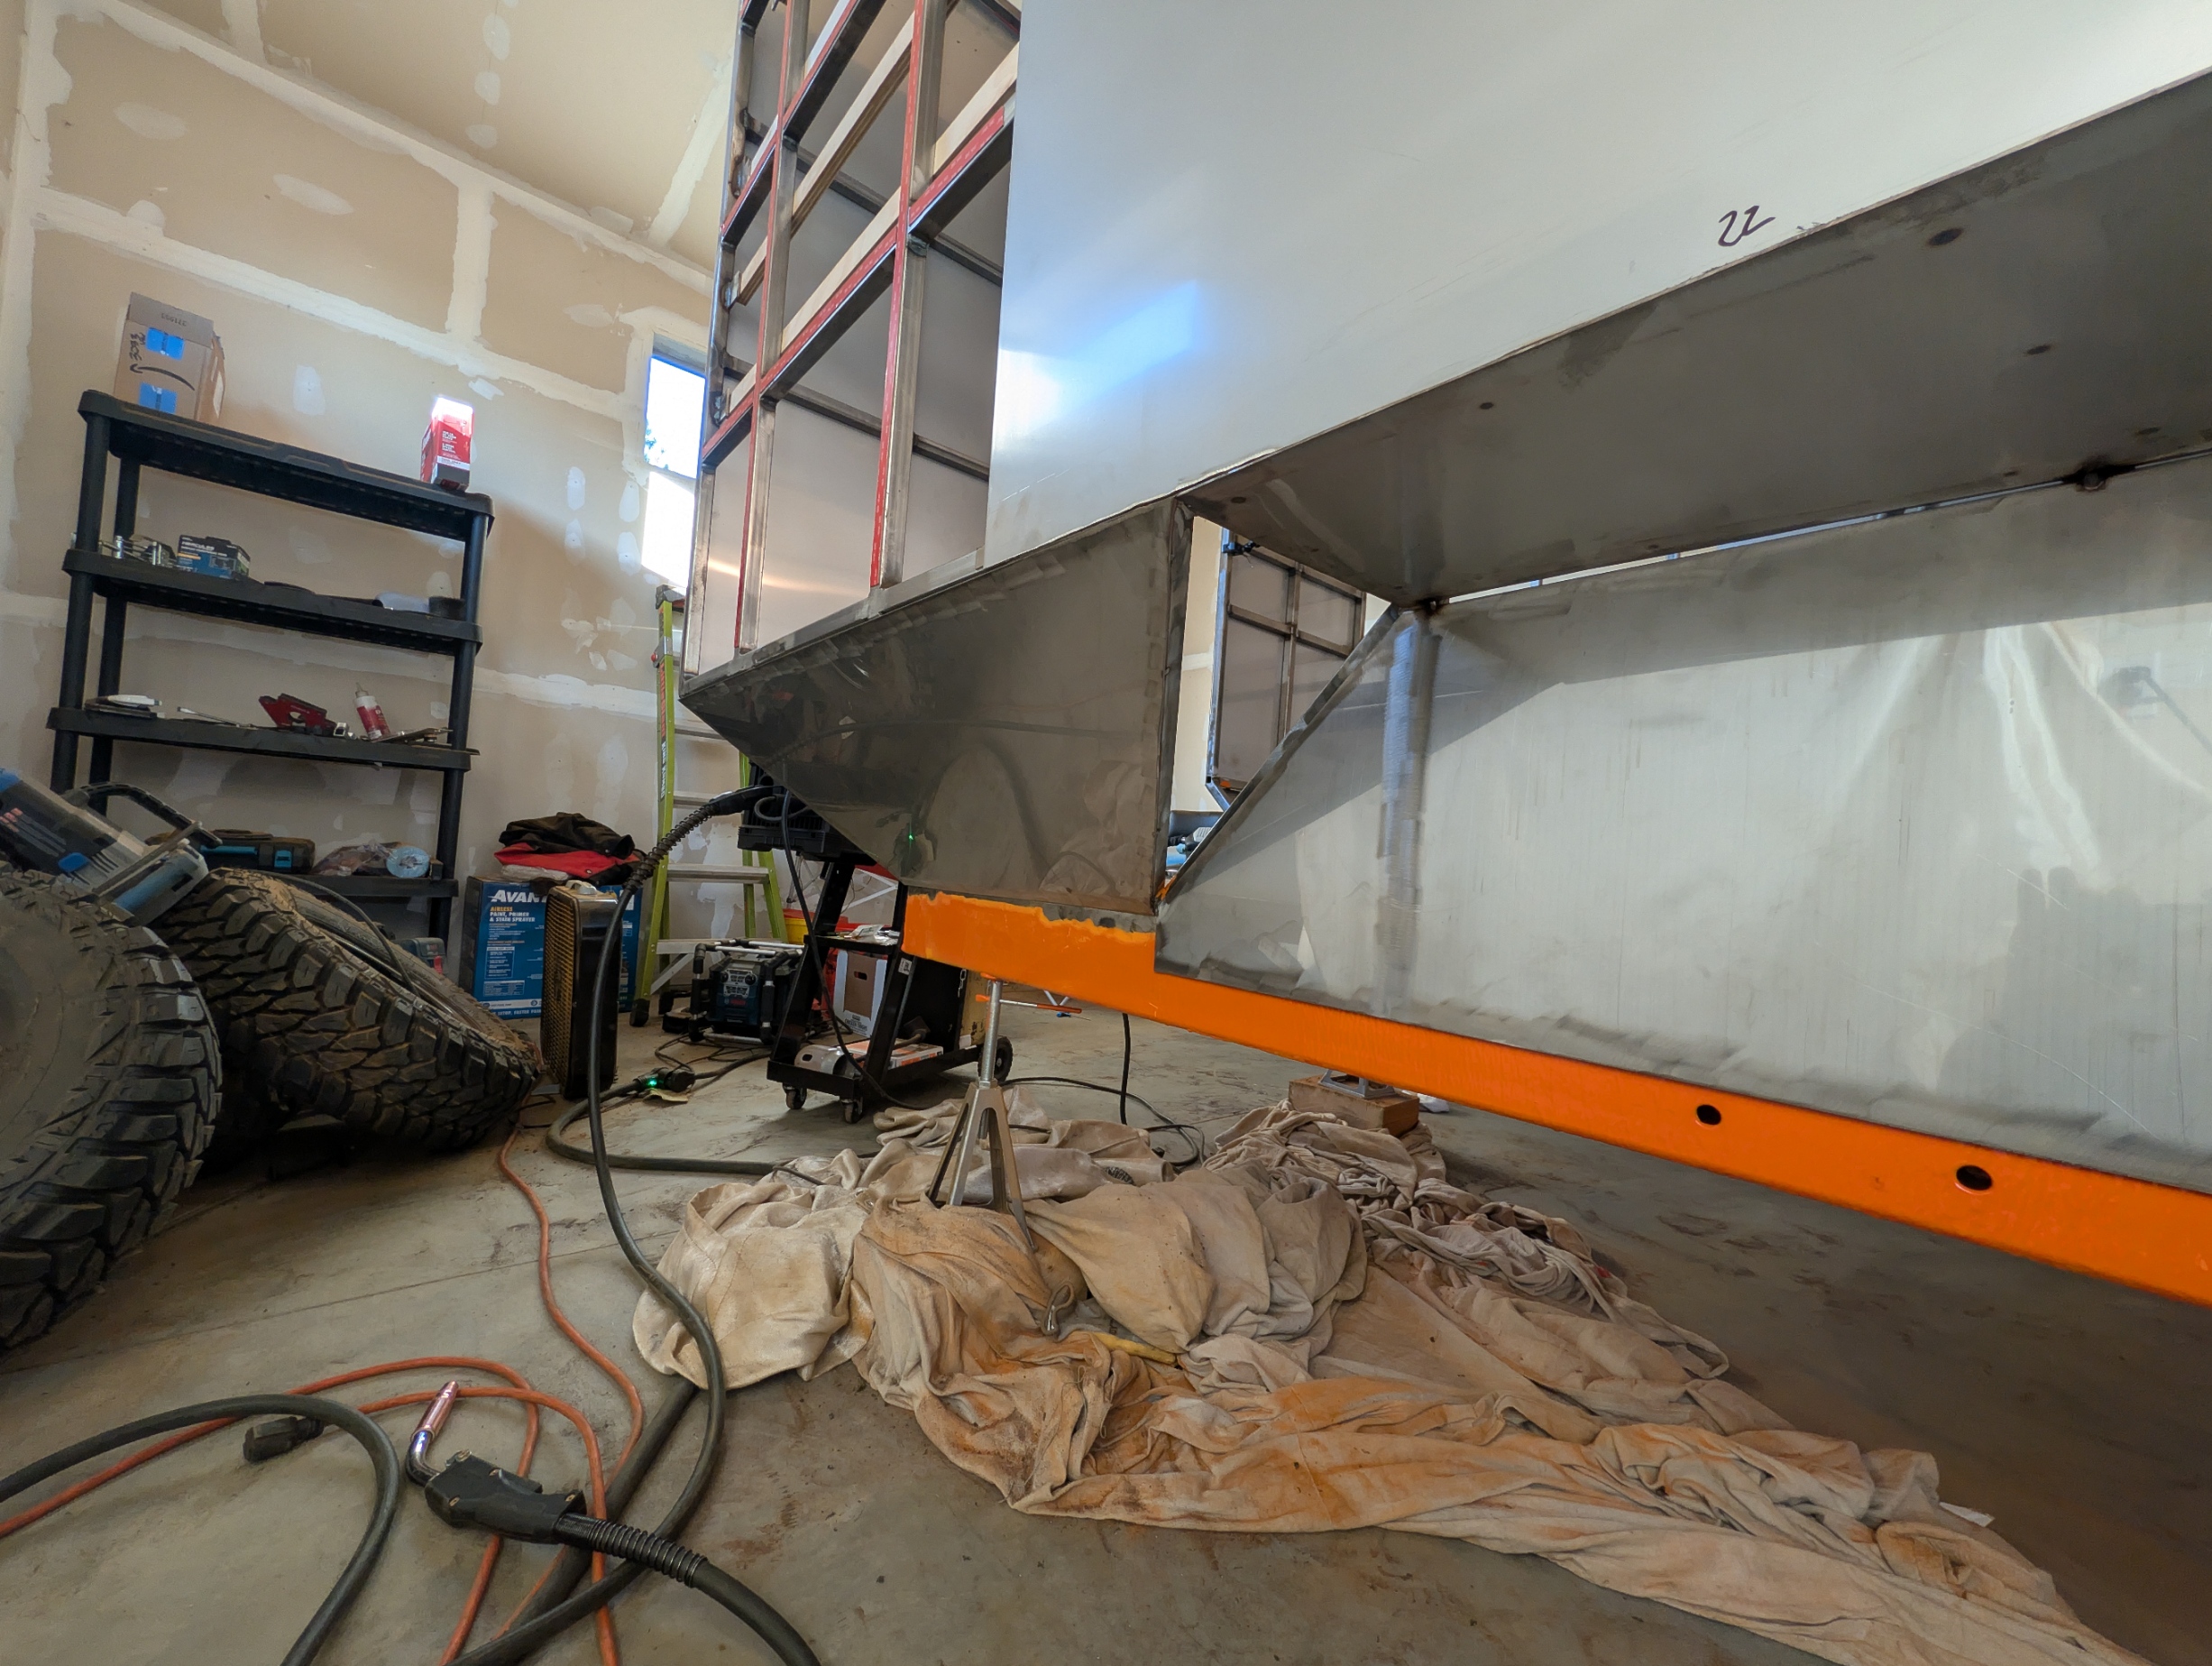
With the help of awesome friends I got the siding panels hung. I then spent a couple days cutting out the trim pieces, labeling everything and then finding a shop that could bend them into 90 or 45° angles as needed. As of today I'm waiting on the trim. Before that I had spent a few days cutting out and fitting up the lower fender panels. As I'm learning in construction or at least in my construction nothing is ever perfect and so fitting panels up always requires some fenagling.
I used the mig welder with a 309L wire (requiring new drive rollers, a new gun liner, new tip) to tack the lower fender panels into place, 304L stainless being non-magnetic is super annoying to hold in place on an angle. In hindsight I should've had the panels bent out of a single piece attached that at the correct angle to the frame with some temporary tubing then used that as a guide to fit my angled frame to make sure the frame was perfect. Almost working backward if you will. WELL I like to do things the most difficult way possible so some framing members are a little out of alignment but nothing some shims and welds can't fix.